

 Español
 عربى
product
product
product
product
product
product
product
product
product
product
product
product
product
product
product
product

Product Category
Contact us
Automotive Bolts And Nuts Suppliers
-
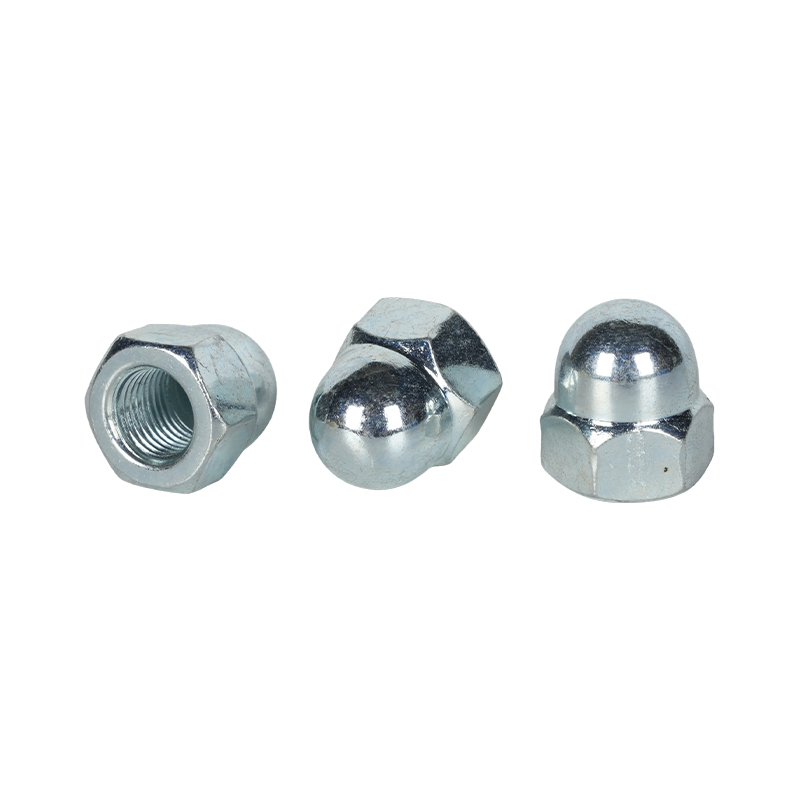
GB/T 802.3 Flange Domed Cap Nut
-
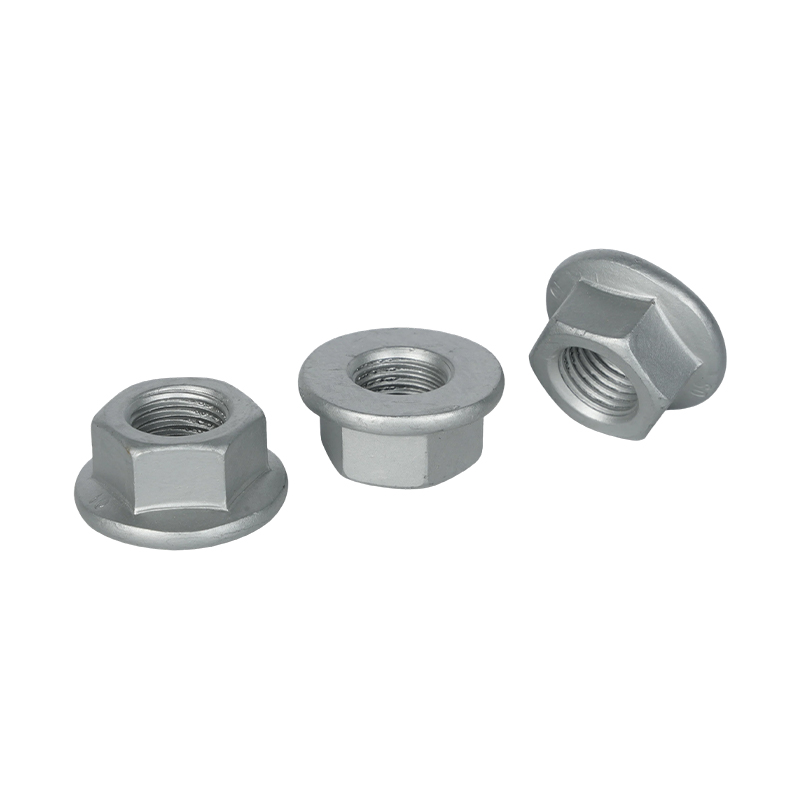
GB/T 6177 Hexagon Nuts with Flange,/DIN6923 Flange nuts with/without serration
-
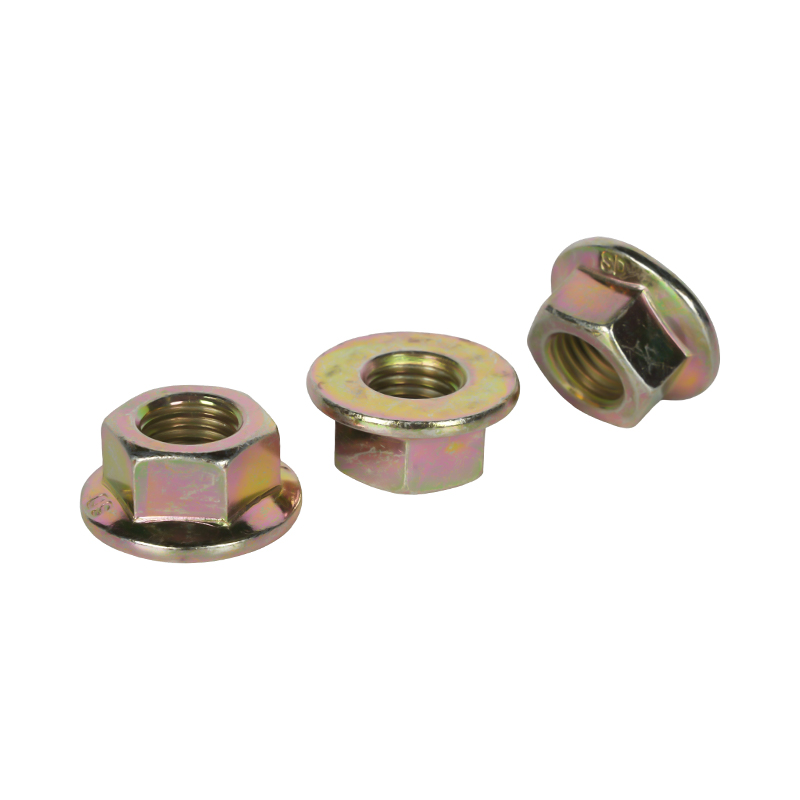
GB/T 6177 Serrated Hexagon Nuts with Flange, /DIN6923 Flange nuts with/without serration Yellow Zinc Plated
-
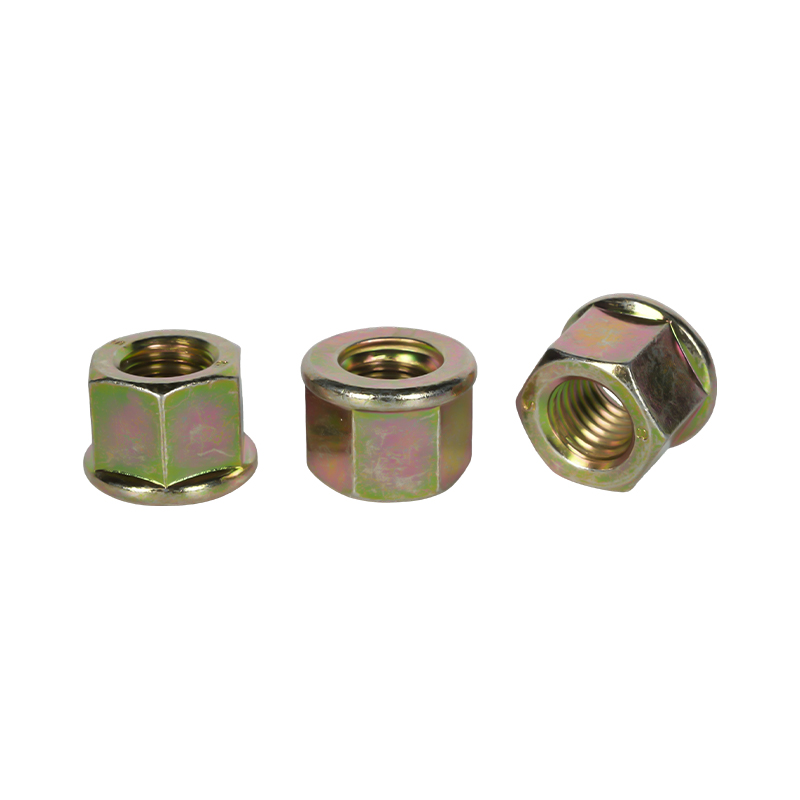
Thick Hex Flange Nuts, Yellow Zinc Plated
-
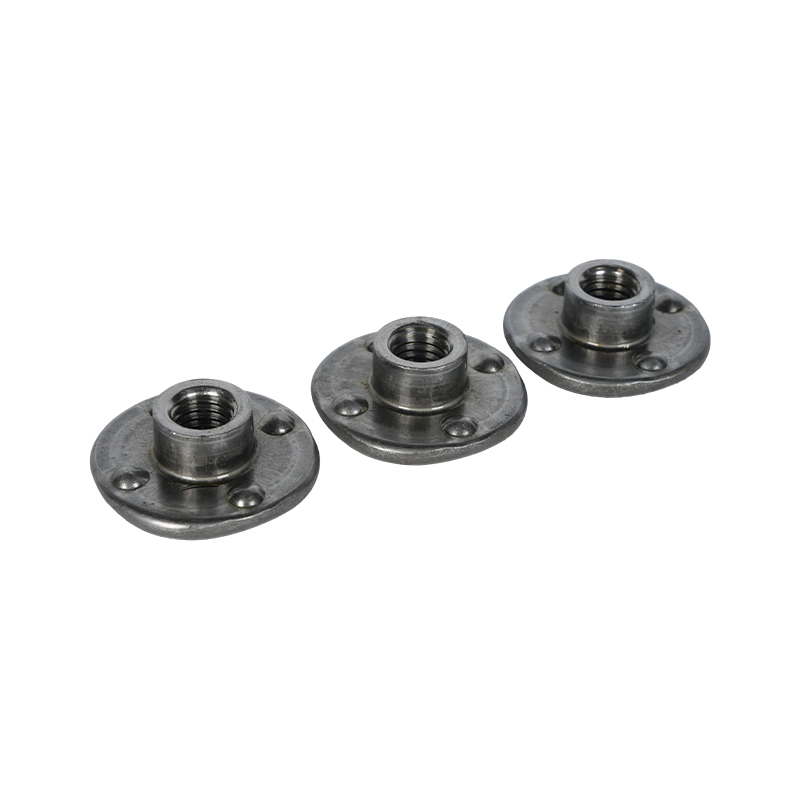
Spot Weld T- Nut
-
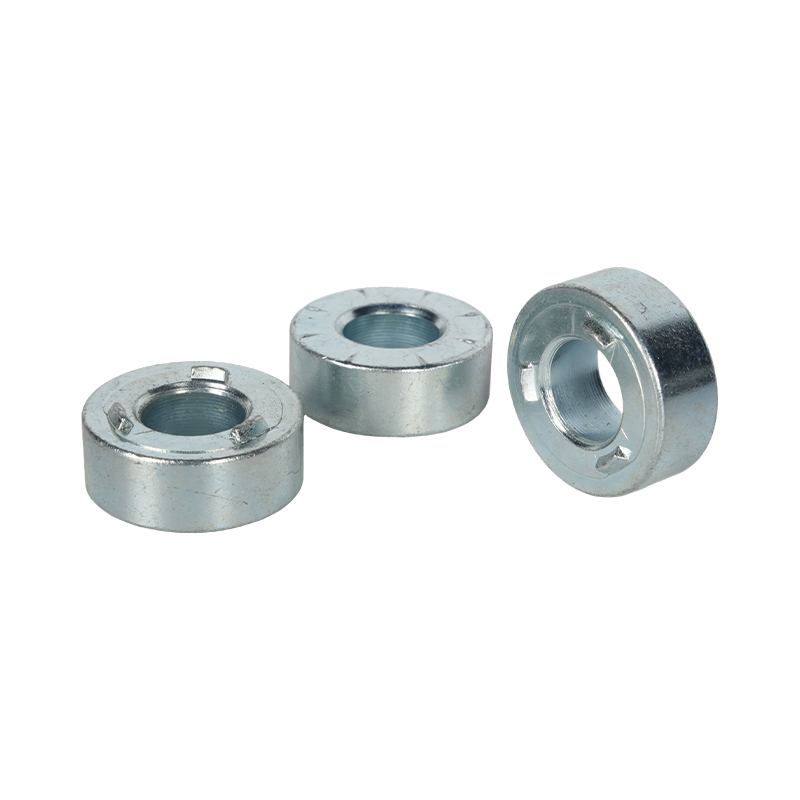
Round Weld Spacer, Zinc Plated
-
Round Weld Spacer with Internal Thread
-
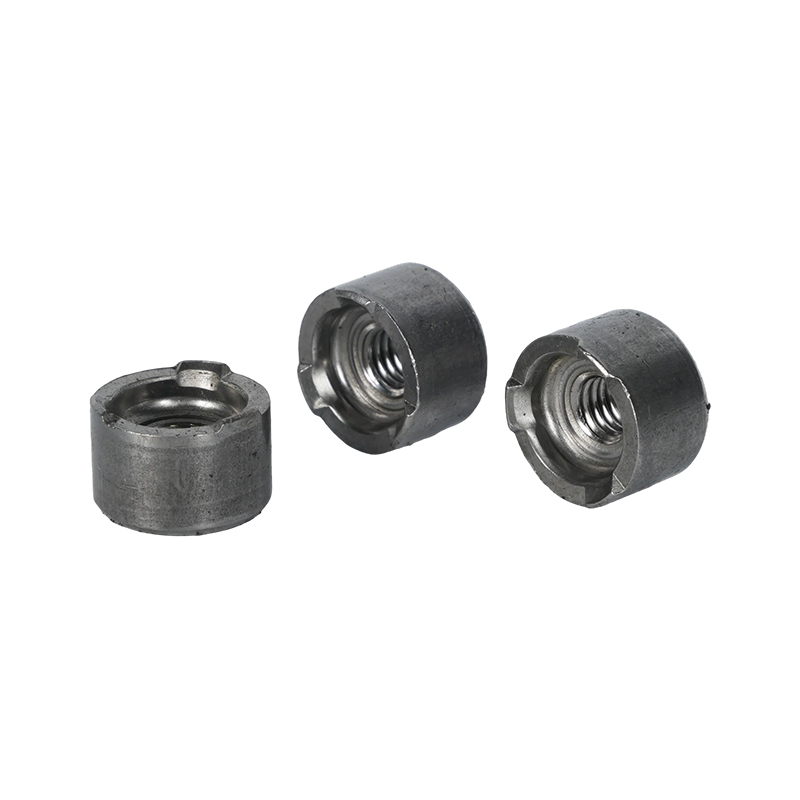
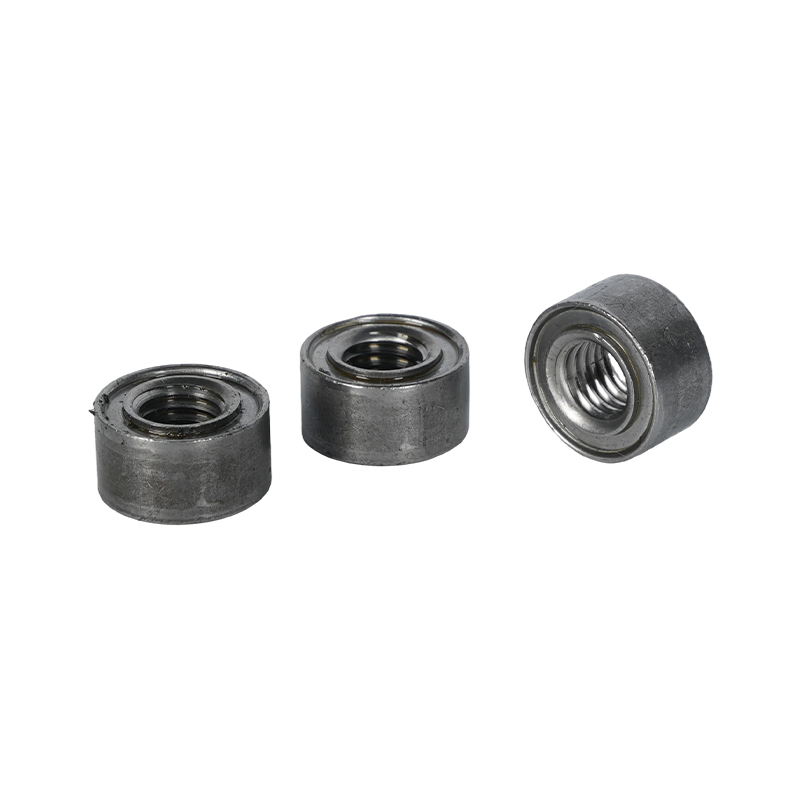
Carbon Steel Round Welded Nut, Cylindrical Welding Nut
-
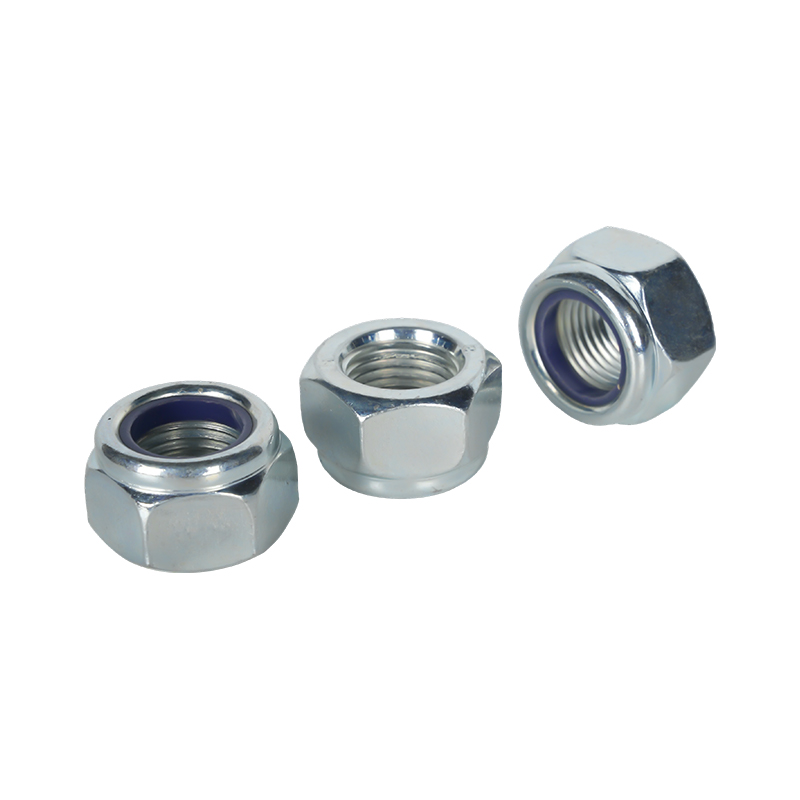
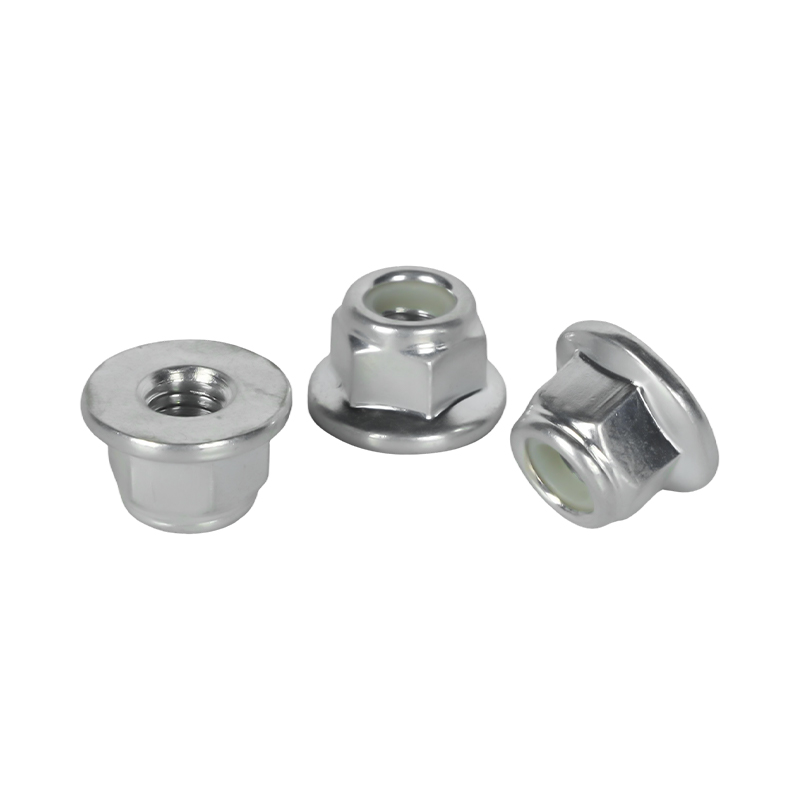
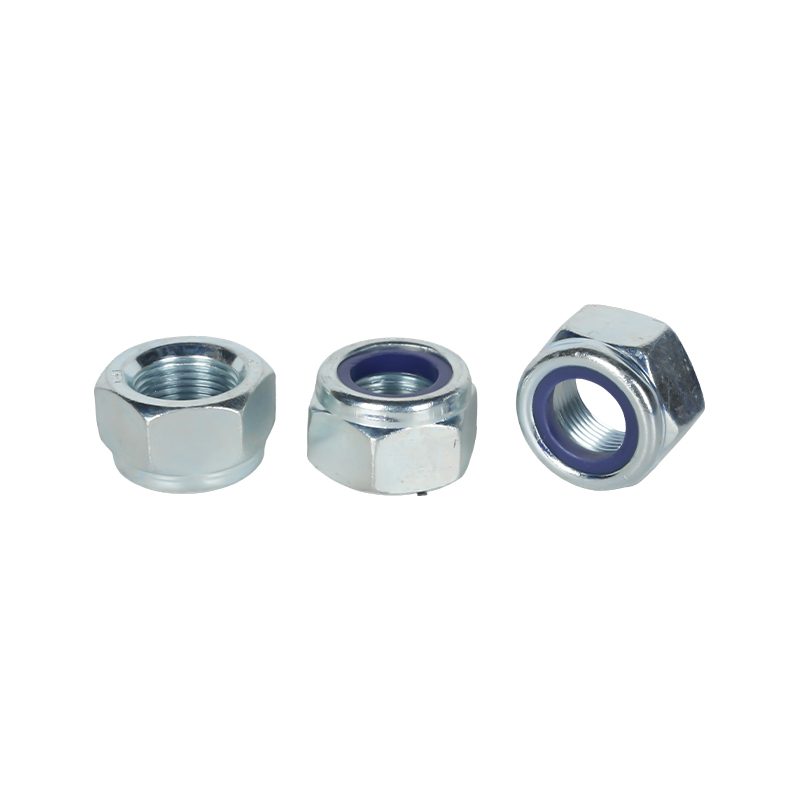
GB/T 6182 Hexagon Nuts with Non-Metallic Insert (Type 2)
-
GB/T 6183 Hexagon Nuts with Non-Metallic Insert (Type 1)/Nylon Insert Lock Nuts
-
GB/T 6182 Hexagon Nuts with Non-Metallic Insert (Type 2)/Nylon Insert Lock Nuts
-
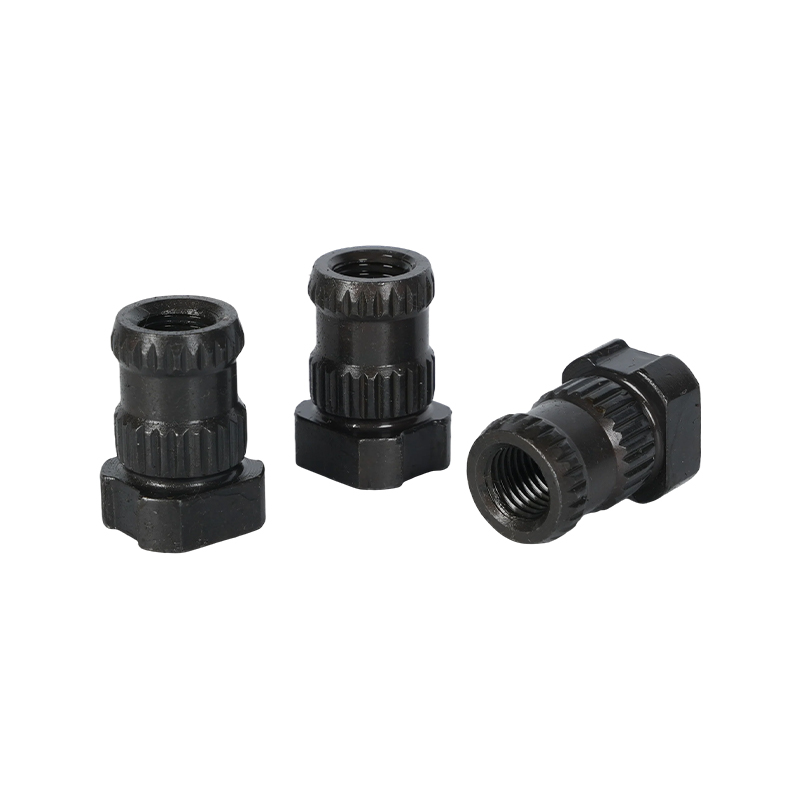
Black Carbon Steel Knurled Serrated Nut
Message Feedback
About Us
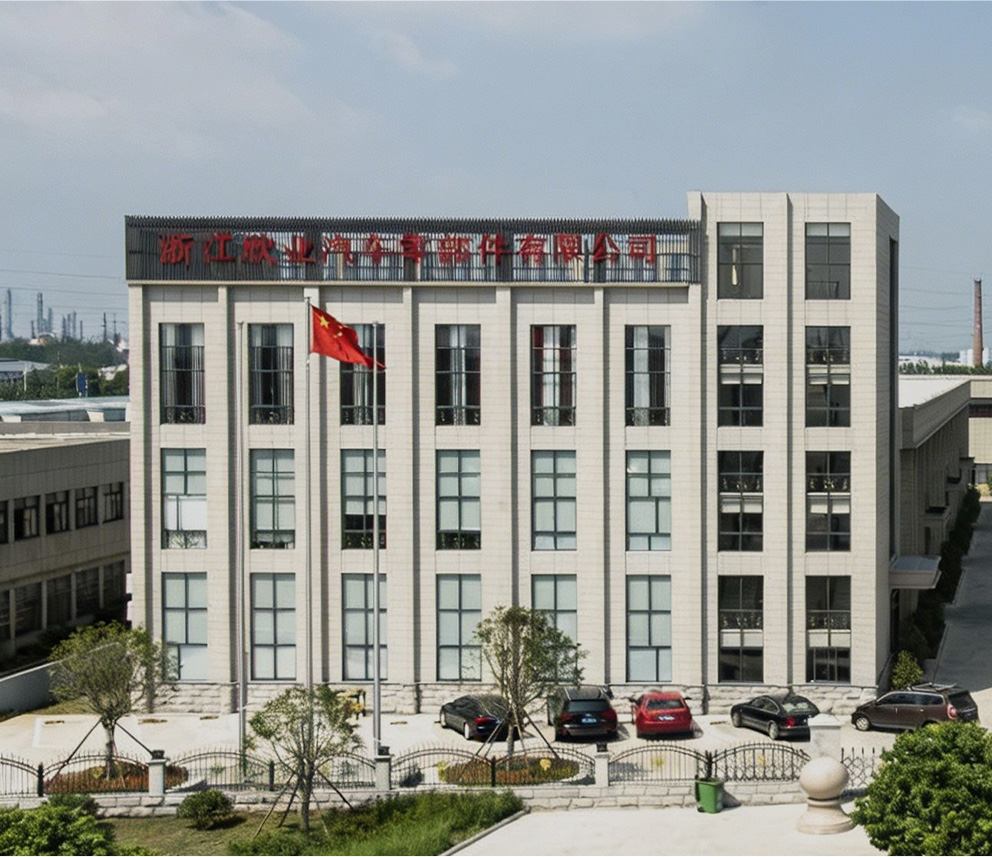
30 Years of Expertise in Automotive Fasteners
Zhejiangxinye Automobile Technology Co. , Ltd. traces its origins to 1995, evolving from Jiaxing Zhapu Xinye Standard Parts Co., Ltd. We are China Car Screw Fasteners Suppliers and Custom
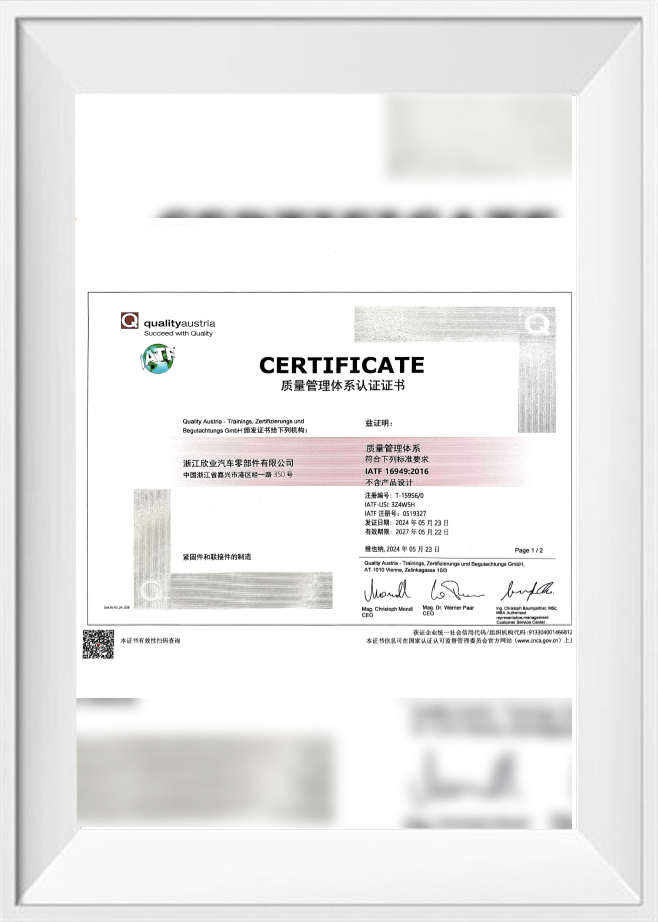
Automotive Bolts And Nuts factory. The company specializes in the production of various automotive fasteners and stamping parts, including flange nuts, welding nuts, and more. For over 30 years, Xinye has kept pace with industry trends, focusing on technological innovation and internal management, and has achieved steady growth. The company is now certified to IATF 16949-2016.
Adhering to the principle of "surviving by product quality, developing by technological innovation," Xinye takes quality as its foundation and customer satisfaction as a top priority, committed to providing suitable and reliable products. To enhance product competitiveness and strengthen employee quality awareness, the company has established a sound management system and standardized process flows. Work instructions have been developed for special and critical processes, and strict quality inspections are conducted at every step. From raw material analysis to finished product mechanical performance testing, process control is implemented to ensure product conformity. The continuously improving quality management system and stable product performance have earned the company market recognition, as well as customer trust and praise.
Adhering to the principle of "surviving by product quality, developing by technological innovation," Xinye takes quality as its foundation and customer satisfaction as a top priority, committed to providing suitable and reliable products. To enhance product competitiveness and strengthen employee quality awareness, the company has established a sound management system and standardized process flows. Work instructions have been developed for special and critical processes, and strict quality inspections are conducted at every step. From raw material analysis to finished product mechanical performance testing, process control is implemented to ensure product conformity. The continuously improving quality management system and stable product performance have earned the company market recognition, as well as customer trust and praise.
-
0m2
Factory Area
-
0
Brand Origin
-
0+
Product Range
Zhejiangxinye Automobile Technology Co. , Ltd.
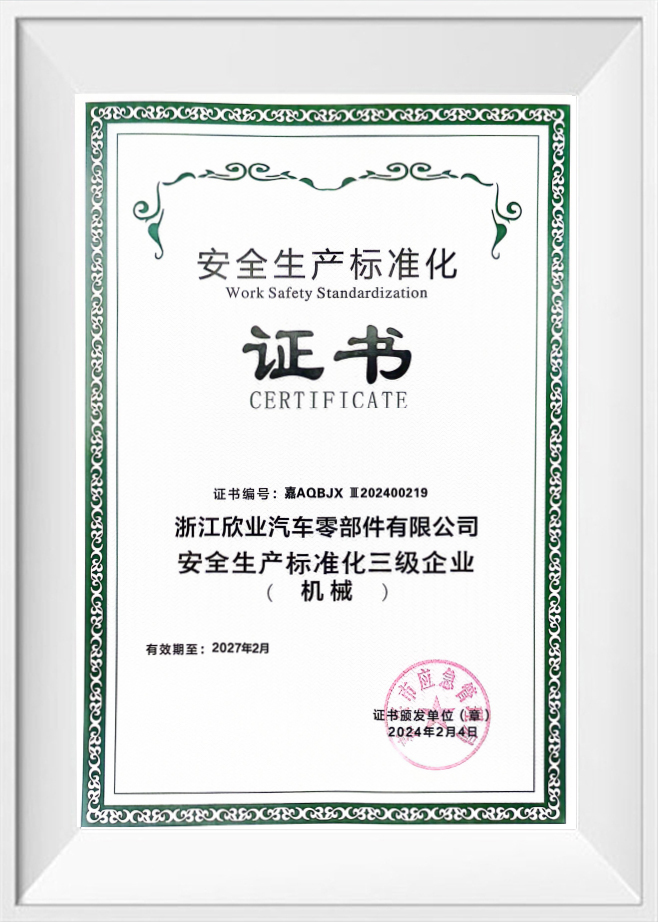
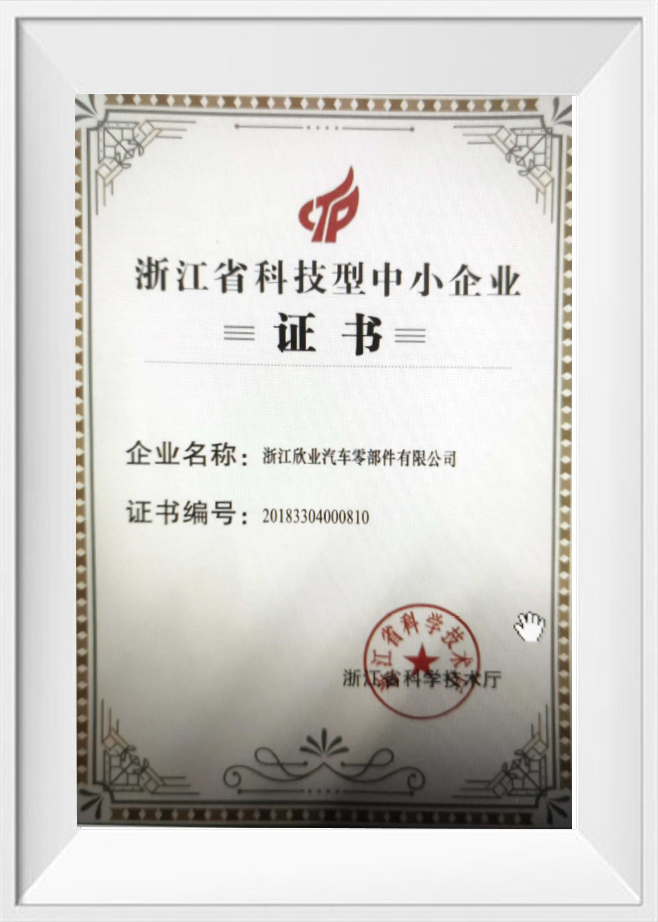
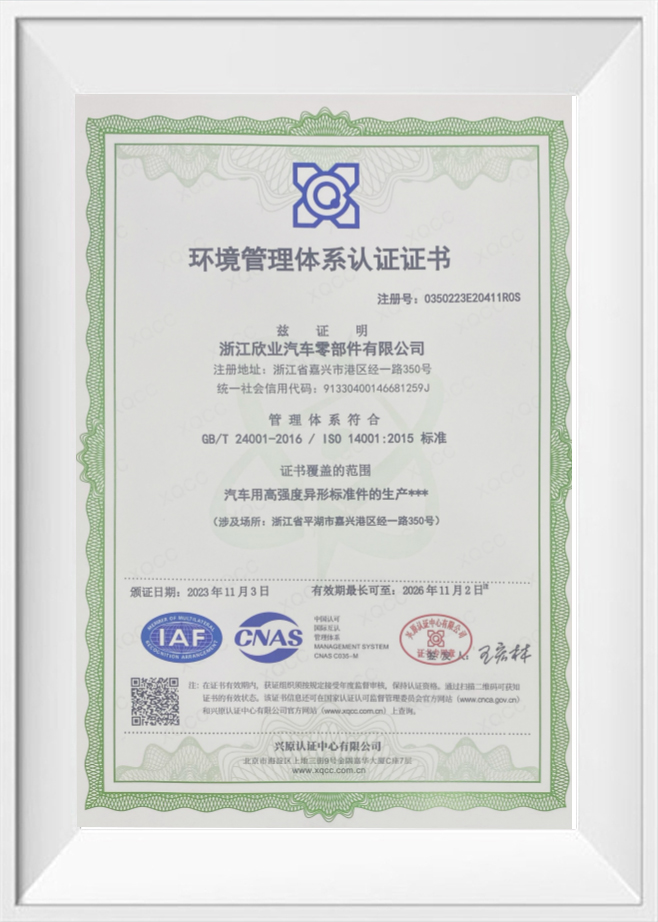
Certificate Of Honor
What’s News
Industry Insights & Updates
View All News
-
2026-11-03Industry News
-
2026-11-03Industry News
-
2026-11-03Industry News
-
2026-11-03Industry News
-
2026-11-03Industry News
-
2026-11-03Industry News
Automotive Bolts And Nuts, Car Screw Fasteners Industry Knowledge
Zhejiangxinye Automobile Technology Co., Ltd. has manufactured automotive fasteners and stamping parts at Jiaxing Port Area, Zhejiang since 1995, and our catalogue now runs beyond 500 product varieties. The range presented here as Automotive Bolts And Nuts Suppliers, Custom Car Screw Fasteners covers the joints that decide body stiffness, seat integrity, battery pack sealing and exhaust durability, produced in-house from raw material through cold heading, thread rolling, heat treatment, finishing and mechanical performance testing.
Our manufacturing position
- IATF 16949-2016 certified automotive fastener manufacturer, established 1995
- Cold heading, tapping, thread rolling, heat treatment and a dedicated surface-finishing line
- Strength grades held from class 5 and 8 up to class 12, with class 13–14 ultra-high-strength development
- Trivalent zinc at 480 h salt spray; Zn–Ni alloy at 480–720 h salt spray
Where Our Fasteners Sit in the Vehicle
Our parts are specified by vehicle system rather than by catalogue page, because the working point — sheet thickness, mating material, access for the assembly tool, corrosion exposure and temperature — decides the geometry as much as the thread size does.
- Body-in-white and closures: spot weld T-nuts, cylindrical weld nuts, weld spacers and flange nuts that create a serviceable thread in thin-gauge panels.
- Seat systems: seat belt nuts, seat system nuts, adjustment shims, spacer nuts and adjuster parts for track and recliner assemblies.
- EV battery pack: sealed nuts that keep the enclosure thread tight against moisture and fluid ingress.
- Powertrain and exhaust: flange and hex nuts in temperature grades up to 650–700 °C for manifold and engine-periphery positions.
- Chassis and wheel end: wheel nuts, thick hex flange nuts and machined sleeves for suspension arm mounting.
- Interior: circlips, springs, knurled insert nuts and clamp components for trim retention.
Our Product Range
Five families cover the fastening and joining scope we produce, and each can be supplied to a documented standard or to your own drawing.
| Product family | Representative parts | Application fit | Configuration levers |
|---|---|---|---|
| Nuts | GB/T 6177 and DIN 6923 flange nuts, thick hex flange nuts, GB/T 802.3 domed cap nuts, weld T-nuts and weld spacers, GB/T 6182 and GB/T 6183 nylon insert lock nuts, knurled, slotted, clinch, sliding and non-standard nuts | Body brackets, weld-on assemblies, threaded inserts in sheet metal, joints that need prevailing torque or a sealed cap | Thread size, strength class, flange serration, weld projection, insert material, plating |
| Bolts & Screws | Custom car screw fasteners, flange and hex bolts, thread-forming and machine screws | Structural, bracket and trim attachment where a matched bolt-and-nut pair is engineered together | Head form, drive, length and thread pitch, class, coating, pre-applied locking patch |
| CNC Machined Components, Sleeves & Pins | Sleeve parts and couplers, pins and shafts, multi-step bushings, precision machined components | Suspension arm mounting, hinge and pivot points, alignment and spacing in welded assemblies | Bore and step geometry, tolerance band, material grade, surface finish |
| Specialty & Functional Automotive Components | Seat belt nuts, seat system nuts, seat adjustment shims and spacer nuts, sealed nuts for EV battery pack, wheel nuts, tow hooks, interior trim circlips and springs | Safety-restraint anchors, towing points, battery enclosure sealing, wheel fixing, seat track adjustment | Thread and seat form, sealing element, load class, plating and colour, assembly orientation |
| Metal Stampings | Brackets, reinforcement plates and functional stampings | Body reinforcement and carrier plates supplied together with the fastener that seats in them | Material thickness, blank geometry, hole pattern, surface treatment |
Strength, Tolerance and Thread Engineering
Class is a design decision, not a label. Our production history runs from class 5 and 8 fasteners to class 12 parts that carry higher axial loads in heavy-duty truck and high-performance engine positions, and class 13–14 ultra-high-strength nuts have completed pre-research for applications where conventional grades run out of margin.
- Tolerance control: thread and dimensional ranges are matched to the joint, with precision control from 0.06 mm to 0.30 mm depending on part size and function.
- MAT self-correcting thread: the first threads guide a slightly misaligned bolt back onto the correct path, which reduces cross-threading stalls on automated assembly lines.
- Flange and serration geometry: flange diameter, serration pattern and bearing face are set against the clamping surface to distribute load and resist loosening.
- Prevailing torque: nylon-insert lock nuts to GB/T 6182 and GB/T 6183 for joints that must stay put under vibration.
Coatings and Temperature Grades
Surface finishing runs on our own line, so corrosion class and heat resistance are selected at the specification stage rather than added afterwards.
| Finish / grade | Verified performance | Typical location |
|---|---|---|
| Trivalent zinc plating | 480 h salt spray | Body, bracket and general chassis fasteners |
| Zn–Ni alloy plating | 480 h to 720 h salt spray | Underbody and high-corrosion zones |
| Yellow zinc plating | Applied to serrated and thick hex flange nuts | General threaded joints with a visible finish requirement |
| Temperature grade 300 °C | Steady performance at rated temperature | Engine periphery, warm brackets |
| Temperature grade 550 °C | Steady performance at rated temperature | Exhaust flanges and hot-side joints |
| Temperature grade 650–700 °C | Steady performance at rated temperature | Manifold and closest-to-source positions |
Process Control and Acceptance
We operate to IATF 16949-2016, and process control starts before the first heading stroke: incoming steel is analysed, then traced through cold heading, tapping, thread rolling, heat treatment and finishing to finished-part mechanical performance testing.
Work instructions are written for the special and critical processes — heat treatment, thread formation, welding geometry on weld nuts and coating — and inspection is placed at each step rather than at the end of the line. Hardness testers sit with the heat-treat operation so grade and case condition are checked against the drawing continuously.
The acceptance scope we agree per part normally covers thread gauging and dimensional layout, hardness and mechanical performance, coating condition, weld or clinch features where applicable, and freedom from burrs on assembly faces.
Information We Use to Configure Your Solution
What to send with an enquiry
- Drawing or standard reference: GB/T, DIN or your own part drawing with revision
- Thread size and pitch, strength class, and the mating bolt or stud specification
- Material and, where it matters, the sheet thickness or host component the part seats in
- Assembly method: robot or hand tool, weld, clinch, press-fit or adhesive
- Corrosion hours and continuous service temperature for the location
- Installation torque target and any prevailing-torque requirement
- Annual volume, call-off pattern and packaging or labelling format
Packaging, Documentation and Supply Scope
Packaging is agreed per order so parts reach the line ready for feeding or kitting rather than being re-handled on arrival. Bulk cartons, bagged quantities, layer pads and label content are confirmed against your incoming-goods process, and mixed shipments of nuts, bolts, machined parts and stampings can be consolidated where a project calls for more than one family.
Alongside the parts, the documentation set is fixed during quotation: the controlling drawing or standard, material and strength grade, coating specification, and the inspection records your receiving inspection needs to release the lot. When a part is developed from a customer drawing rather than a published standard, the drawing revision governs the acceptance criteria for the life of the programme.
Frequently Asked Questions
What does Zhejiangxinye Automobile Technology manufacture?
We produce automotive fasteners and stamping parts: nuts, bolts and screws, CNC machined sleeves, pins and precision components, functional body, seat and battery hardware, and metal stampings. Production is completed in-house from raw material to finished goods across more than 500 product varieties.
Can you make a custom car screw fastener with no GB/T or DIN equivalent?
Yes. Our non-standard nuts and custom screw fasteners are built from the customer drawing. Send the drawing, thread specification, strength class, material, coating, mating part and annual volume and we configure the head form, thread, bearing face and finish around that working point.
Which strength classes and thread tolerances do you hold?
Production covers classes from 5 and 8 through class 12, with class 13–14 ultra-high-strength nuts developed for higher axial loads. Dimensional and thread tolerance ranges are controlled between 0.06 mm and 0.30 mm, selected according to part size and joint function.
How are fasteners specified for corrosive or high-temperature locations?
Trivalent zinc plating is rated at 480 h salt spray and Zn–Ni alloy plating at 480–720 h. For heat, we supply three temperature grades at 300 °C, 550 °C and 650–700 °C, which is how exhaust system and engine-periphery joints are matched to their service environment.
How does a project move from drawing to accepted delivery?
We review the drawing and working point, confirm material, class, coating and acceptance criteria, then run production under documented work instructions for the critical processes. Parts are inspected at each stage, from incoming steel analysis and hardness testing through finished-part mechanical performance checks, before the agreed packaging and documentation are released.
Do you supply mating parts as a set rather than single items?
Where a joint needs a matched pair, we engineer the bolt or screw against the nut, sleeve or stamped plate it seats in — flange geometry, thread fit, strength grade and coating are aligned so the assembly behaves as one system rather than as separately sourced hardware.
- Contact Us
-
-
861260628@qq.com

zj@xy-nuts.com -
+86 15888350558

-
No.350 Jingyi Road, Jiaxing Port Area, Zhejiang Province, China.

-
- Quick Links
- Products
- About Us
- Capabilities
- Service
- News
- Contact Us
- Product
- Nuts
- CNC Machined Components, Sleeves & Pins
- Specialty & Functional Automotive Components
- Metal Stampings
- Bolts & Screws
- Mobile
Copyright ©
Zhejiangxinye Automobile Technology Co. , Ltd.
All Rights Reserved
Custom
Automotive Bolts And Nuts Suppliers
