

 Español
 عربى
product
product
product
product
product
product
product
product
product
product
product
product
product
product
product
product

Product Category
Contact us
Message Feedback
About Us
30 Years of Expertise in Automotive Fasteners
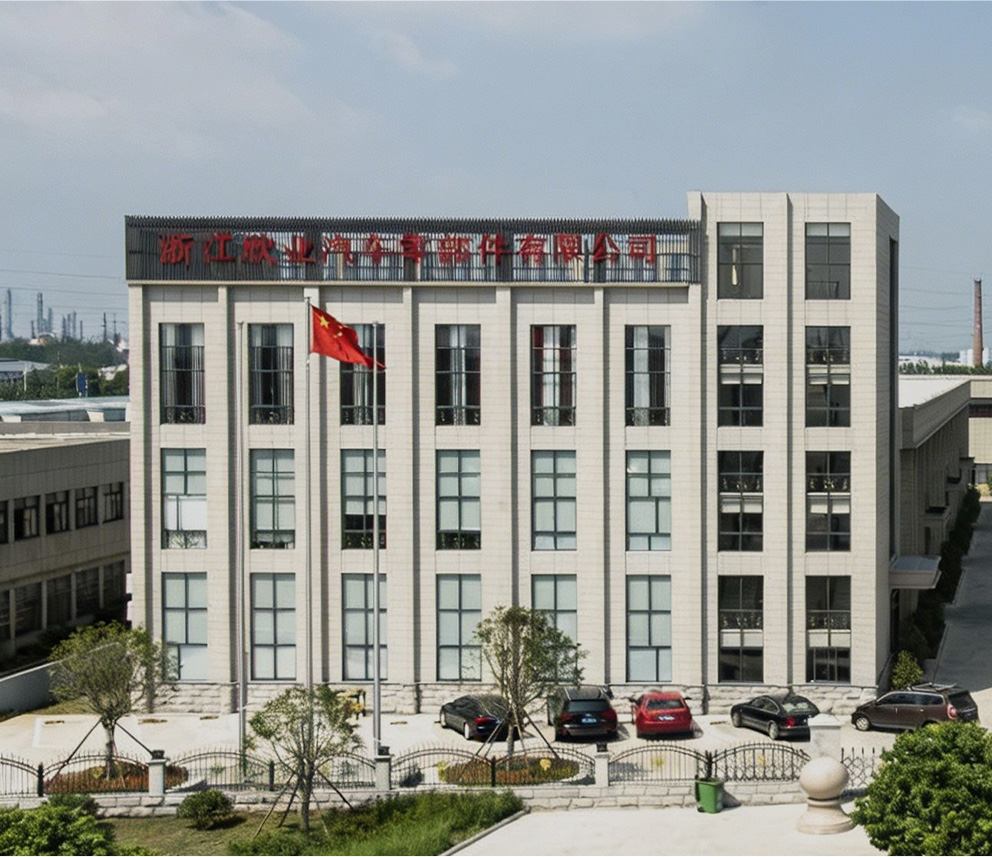
Zhejiangxinye Automobile Technology Co. , Ltd. traces its origins to 1995, evolving from Jiaxing Zhapu Xinye Standard Parts Co., Ltd. We are China High Precision Stamping Suppliers and Custom
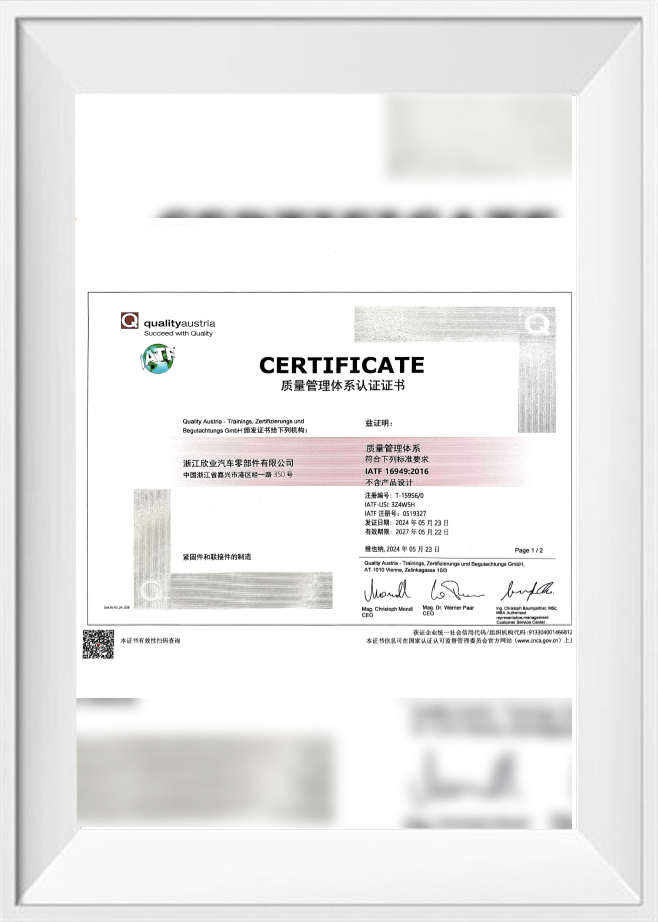
Sheet Metal Stamping factory. The company specializes in the production of various automotive fasteners and stamping parts, including flange nuts, welding nuts, and more. For over 30 years, Xinye has kept pace with industry trends, focusing on technological innovation and internal management, and has achieved steady growth. The company is now certified to IATF 16949-2016.
Adhering to the principle of "surviving by product quality, developing by technological innovation," Xinye takes quality as its foundation and customer satisfaction as a top priority, committed to providing suitable and reliable products. To enhance product competitiveness and strengthen employee quality awareness, the company has established a sound management system and standardized process flows. Work instructions have been developed for special and critical processes, and strict quality inspections are conducted at every step. From raw material analysis to finished product mechanical performance testing, process control is implemented to ensure product conformity. The continuously improving quality management system and stable product performance have earned the company market recognition, as well as customer trust and praise.
Adhering to the principle of "surviving by product quality, developing by technological innovation," Xinye takes quality as its foundation and customer satisfaction as a top priority, committed to providing suitable and reliable products. To enhance product competitiveness and strengthen employee quality awareness, the company has established a sound management system and standardized process flows. Work instructions have been developed for special and critical processes, and strict quality inspections are conducted at every step. From raw material analysis to finished product mechanical performance testing, process control is implemented to ensure product conformity. The continuously improving quality management system and stable product performance have earned the company market recognition, as well as customer trust and praise.
-
0m2
Factory Area
-
0
Brand Origin
-
0+
Product Range
Zhejiangxinye Automobile Technology Co. , Ltd.
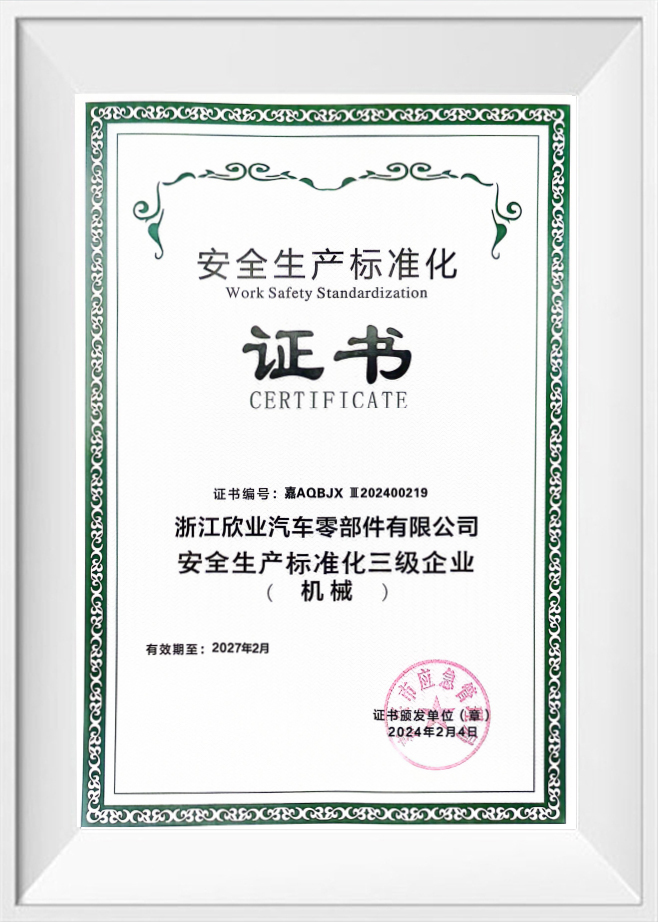
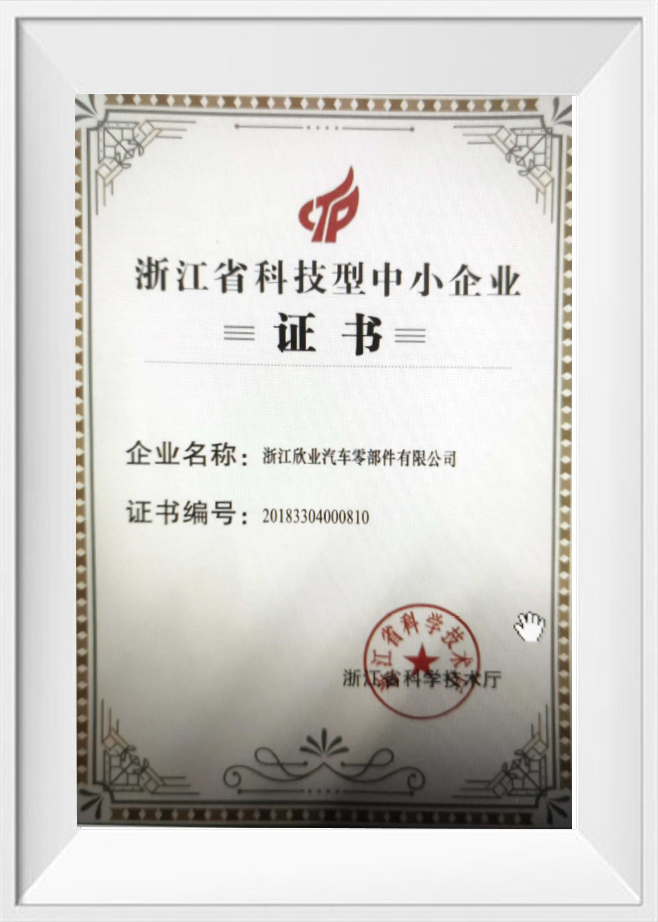
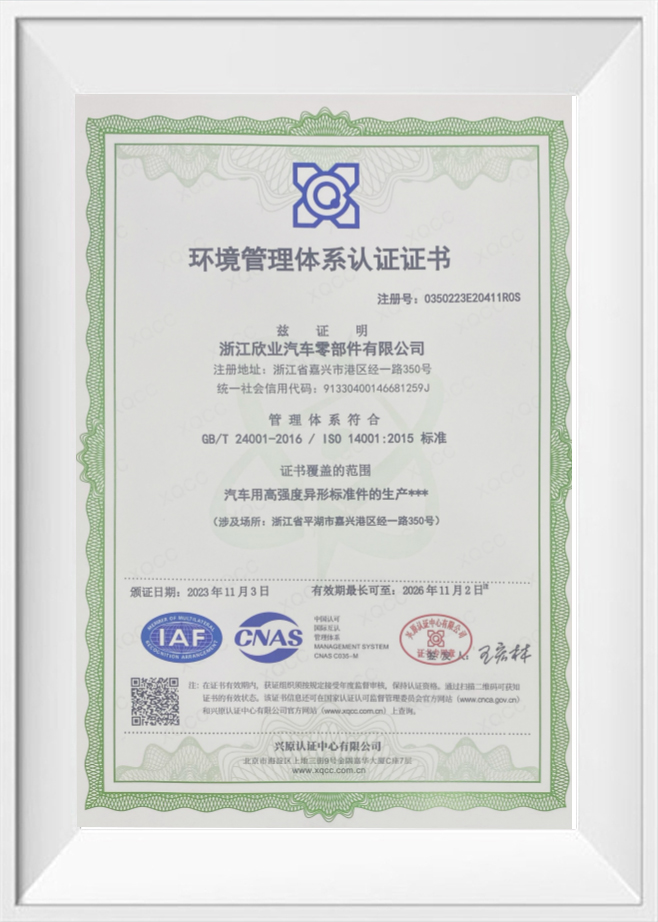
Certificate Of Honor
What’s News
Industry Insights & Updates
View All News
-
2026-11-03Industry News
-
2026-11-03Industry News
-
2026-11-03Industry News
-
2026-11-03Industry News
Metal Stampings Industry Knowledge
Zhejiangxinye Automobile Technology Co., Ltd. manufactures stamped metal fasteners and formed hardware for automotive assemblies, produced alongside our nut, bolt, screw and machined-component ranges. The company traces its origins to 1995 and has worked in automotive fasteners and stamping parts for more than 30 years; production runs from our plant at No.350 Jingyi Road, Jiaxing Port Area, Zhejiang Province, under IATF 16949-2016 certification.
Inside the metal stampings category we supply clip nuts, weld hooks and drawn stamped nuts — parts that combine a formed spring or weld interface with a threaded or retaining function. Each item is built to a customer drawing: strip or wire grade, thickness, formed geometry, thread size, coating system and inspection criteria are fixed before a sample leaves the tool.
Our Stamped Metal Range
Four stamped families cover the majority of the joints our customers bring to us, each with a defined installation method and a defined failure mode to control.
| Stamped product | Construction | Material and finish | Where it fits |
|---|---|---|---|
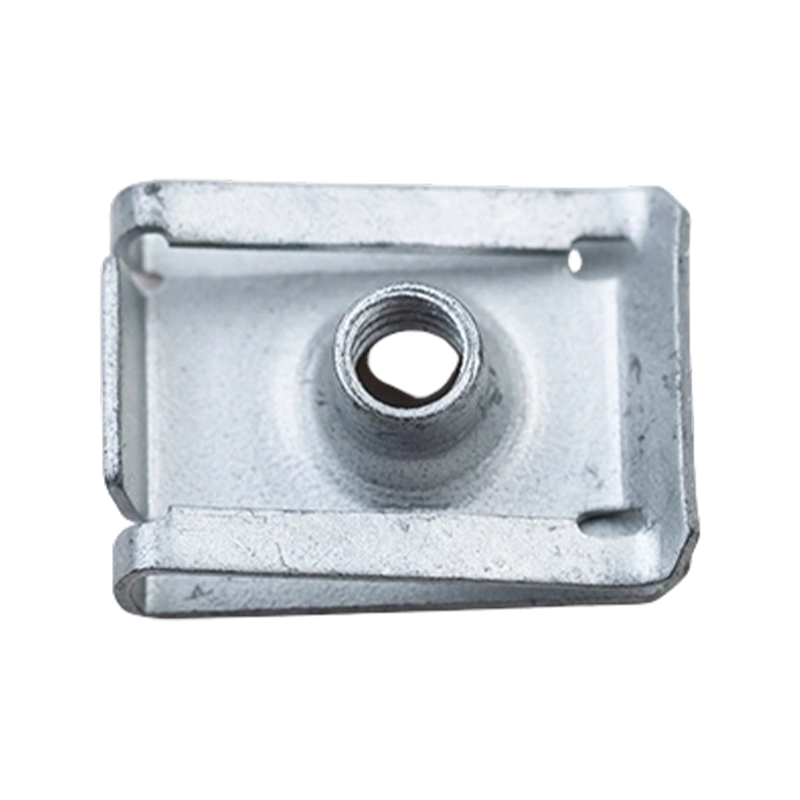
| U-Type Clip Nut With Integrated Tapped Barrel | One-piece spring clip with a drawn barrel carrying 5–10 thread turns | Spring steel 65Mn or SK5; zinc plating, phosphate or black finish | Interior trim, body panels, electrical enclosures, HVAC housings; M3–M12 and #4-40 to 1/2-13 |
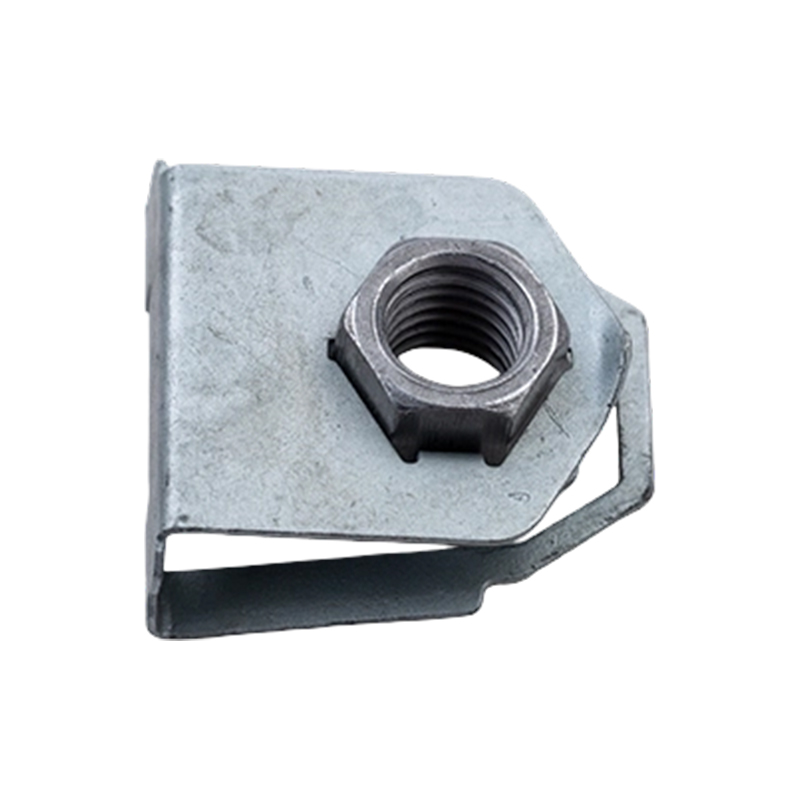
| Galvanized U Clip Spring Nut | U-shaped clip sliding over a panel edge or into an opening | 65Mn spring steel; hot-dip or electro galvanized, zinc plated | Door trims, bumpers, fenders, appliance and furniture panels; M3–M10, typical panel 1–2 mm |
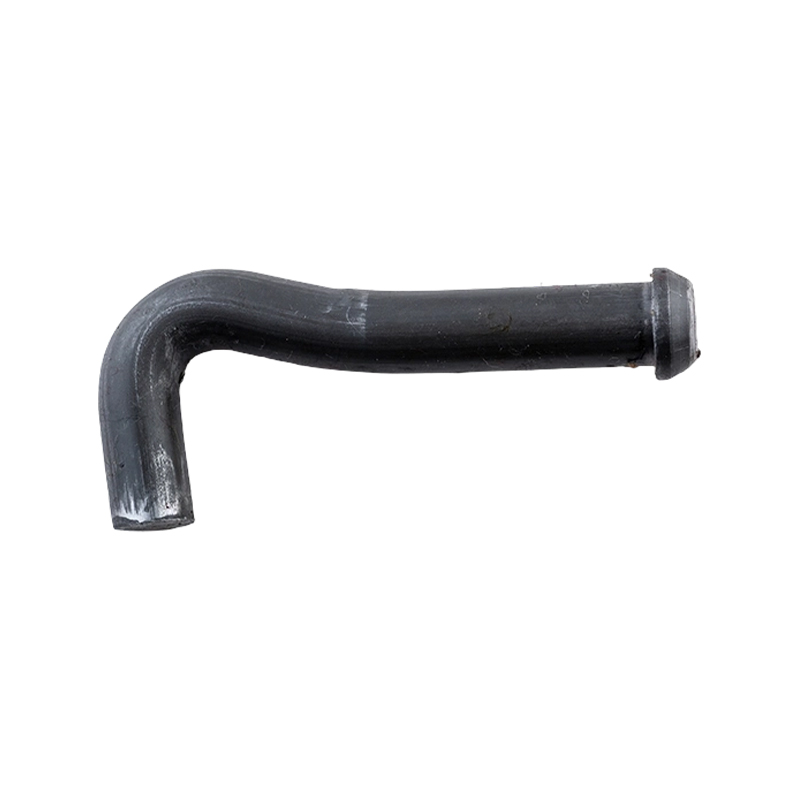
| Carbon Steel L Shape Bent Weld Hook | 90° bent hook with a straight weld leg and retaining end | Carbon steel or stainless; zinc, galvanizing, phosphate | Exhaust hangers, insulation and cladding support, equipment mounting points |
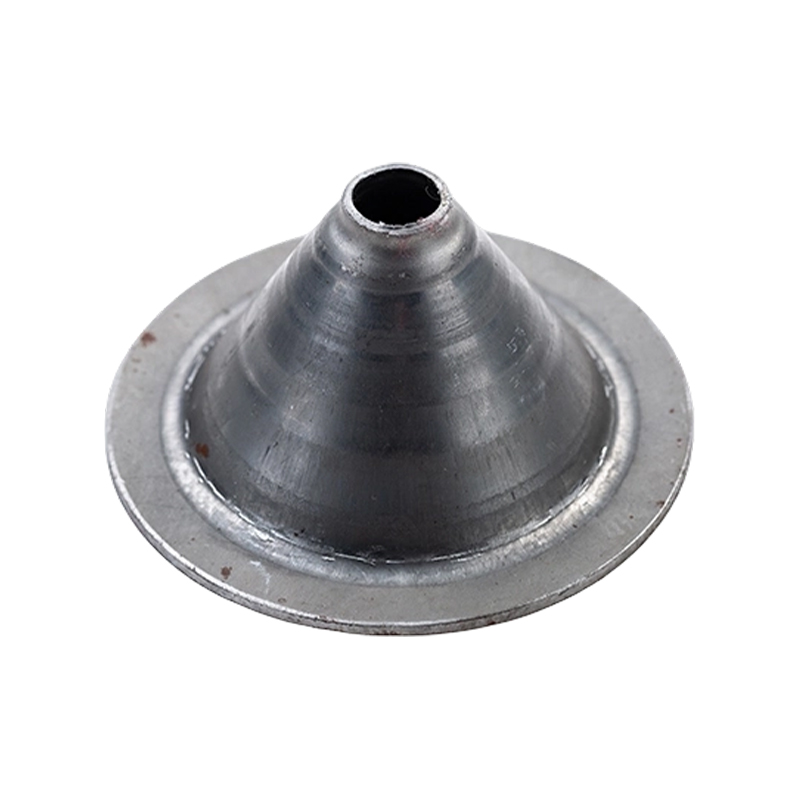
| Carbon Steel Taper Conical Drawn Stamped Nut With Outer Flange | Drawn conical body with outer flange and tapped bore | Carbon steel; coating selected to the exposure zone | Threaded seats in body structures, welded assemblies, seat and trim mountings |
Stamped joints rarely stand alone. Where a project needs a welded or clinched threaded element beside the stamping, our weld nuts, clinch nuts and seat-system parts are produced in the same plant, so thread, coating and material grades stay consistent across the assembly.
Application Fit Across Vehicle and Equipment Assemblies
Stamped clip nuts solve a specific problem: a threaded receptacle is needed on thin sheet metal where the reverse side is closed, painted or simply out of reach. The clip is pressed onto the panel edge or into an opening and stays in position by spring tension until the screw is driven — no welding, no riveting, no tapping of the panel.
- Automotive trim and body. Door trims, fenders, bumpers and pillar covers use the galvanized U clip spring nut where fast assembly and blind-side fixing matter more than high torque.
- Structural and heavier trim joints. The U-type clip nut with integrated tapped barrel carries multiple thread turns, so pull-out resistance and repeated disassembly are better than a flat stamped thread allows.
- Thermal and exhaust zones. L-shape bent weld hooks hold rubber hangers, heat shields and insulation cladding; material and coating are selected for the temperature band and road exposure of that zone.
- Adjacent markets. Electrical enclosures, control cabinets, HVAC housings, appliance panels and modular furniture use the same clip geometry with different spring arms and thread sizes.
Because clip nuts are removable, field service and rework are practical: the clip is compressed or slid off the panel edge and repositioned, unlike a welded nut that requires destructive removal.
Materials and Surface Systems
Spring steel grades such as 65Mn and SK5 give the retention force that keeps a clip on the panel; stainless grades are used where corrosion resistance outweighs spring economy. Carbon steel covers hooks and drawn nuts, with weldability controlled through material composition.
| Finish system | Behaviour | Typical stamped parts |
|---|---|---|
| Trivalent zinc plating | Zinc barrier layer, tested to 480 h salt spray | Clip nuts, hooks, general brackets |
| Zn-Ni alloy plating | 480–720 h salt spray for underbody and exposed hardware | Body-mount clips, weld hooks |
| Galvanizing | Uniform zinc layer with defined thickness | Panel spring nuts, low-cost corrosion protection |
| Phosphate / black finish | Mild protection in dry interior conditions; dark cosmetic appearance | Interior clips, visible trim parts |
| High-temperature grades | Service bands at 300 °C, 550 °C and 650–700 °C | Exhaust hangers, engine-periphery hooks and nuts |
Critical Specifications We Hold on Stamped Parts
- Dimensional tolerance. Feature tolerances are set between 0.06 mm and 0.30 mm according to function — barrel position and flange concentricity tighten, while trim clearances open.
- Thread engagement. A tapped barrel delivers 5–10 usable turns against 2–4 in flat stamped threads, which governs torque capacity and pull-out strength.
- Spring behaviour. Arm geometry is dimensioned to the panel thickness range so the clip holds position before the screw is driven and does not relax in service.
- Formed geometry. Bend angle, leg length, hook radius and weld-leg flatness are inspected against the drawing, since these define orientation in the fixture.
- Weld compatibility. Contact face area and cross-section of the weld leg are matched to resistance or projection welding parameters agreed with the customer's process.
- Mechanical class. Threaded stamped parts are supplied in strength classes up to Class 12 where the joint carries axial load.
Our MAT self-correcting thread technology, applied to threaded products, guides a slightly misaligned bolt back onto the correct thread path in automated assembly — a practical gain where robots or multi-spindle drivers position the screw.
Quality Control and Acceptance
Our system is certified to IATF 16949-2016 and structured around documented work instructions for special and critical processes, with inspection at each production step rather than only at final packing.
- Raw material analysis before release to production, including composition checks against the specified grade.
- In-process checks on formed geometry, thread condition and spring arms, recorded against the control plan for the part.
- Finished-product mechanical performance testing, including hardness verification on heat-treated items.
- Coating verification — thickness measurement and salt-spray evaluation matched to the specified corrosion band.
- First-article and sample approval before series production, with the inspection report issued against the drawing dimensions.
Clips from a batch must interchange with the customer's fixture: spring arms, barrel height and thread start are held so that a clip from any carton seats the same way on the same panel.
Information We Use to Configure Your Solution
A stamping quotation is only as good as the input. We ask for the following so the tool, material and coating are defined in one pass:
- Drawing with material grade, strip or wire thickness, formed dimensions and tolerances.
- For clip nuts: panel thickness range, edge or hole mounting, and thread size and class.
- For weld parts: welding method, electrode access and the mating panel material and thickness.
- Coating specification and required salt-spray duration; service temperature where exhaust or engine heat applies.
- Assembly method — manual, robotic or multi-spindle — and whether repeated disassembly is expected.
- Annual volume, release schedule, pack quantity and carton marking requirements.
- Documentation set required by the programme, including whether production-part approval is needed.
We confirm feasibility against our forming, tapping, heat-treatment and coating routes, then return a configuration covering part geometry, material, finish, inspection plan, packaging and delivery scope for approval before tooling starts. The full range sits alongside our other stamped and threaded lines, including Custom Sheet Metal Stamping, High Precision Stamping Suppliers production and the specialty and functional automotive components built for seat, battery-pack and body applications.
Frequently Asked Questions
What stamped parts does Zhejiangxinye manufacture?
We produce clip nuts with flat or tapped-barrel threads, galvanized U clip spring nuts, L-shape bent weld hooks and conical drawn stamped nuts with outer flanges, all from automotive-grade strip and wire. They are supplied alongside our nut, bolt, screw and CNC machined component ranges.
Can clip nuts be fitted without access to the back of the panel?
Yes. The U-shaped clip slides over the panel edge or into an opening and holds itself by spring tension, creating a threaded receptacle from one side only. Welding, riveting or tapping of the panel is not required, and the clip can be compressed and removed if the joint has to be repositioned.
What thread sizes and panel thicknesses are available?
Clip nut threads run from M3 to M12 in metric and #4-40 to 1/2-13 in unified profiles. Panel thickness compatibility is set by the spring arm geometry; standard galvanized U clips are typically used on 1–2 mm sheet, and arms are dimensioned to the actual panel range on custom parts.
Which coatings and temperature grades do you offer?
Trivalent zinc plating tested to 480 h salt spray, Zn-Ni alloy plating at 480–720 h, galvanizing, phosphate and black finishes are available. For exhaust and engine-periphery positions we supply parts in three temperature grades covering 300 °C, 550 °C and 650–700 °C service.
How do weld hooks attach, and are they removable?
The straight leg is welded to the workpiece by resistance, projection or another process compatible with the material grade, and the perpendicular end acts as the hook or retaining feature. Installation is permanent; removal requires grinding or cutting, so the weld position is fixed at drawing approval.
What do you need to quote a custom stamping?
A dimensioned drawing with material and thickness, the mating panel or weld details, thread and coating requirements, service temperature, assembly method, annual volume and packing instructions. With those inputs we define the configuration, inspection plan and delivery scope and issue a quotation against them.
- Contact Us
-
-
861260628@qq.com

zj@xy-nuts.com -
+86 15888350558

-
No.350 Jingyi Road, Jiaxing Port Area, Zhejiang Province, China.

-
- Quick Links
- Products
- About Us
- Capabilities
- Service
- News
- Contact Us
- Product
- Nuts
- CNC Machined Components, Sleeves & Pins
- Specialty & Functional Automotive Components
- Metal Stampings
- Bolts & Screws
- Mobile
Copyright ©
Zhejiangxinye Automobile Technology Co. , Ltd.
All Rights Reserved
Custom
Sheet Metal Stamping Suppliers
