

 Español
 عربى
product
product
product
product
product
product
product
product
product
product
product
product
product
product
product
product

Product Category
Contact us
Auto Body Nuts Suppliers
-
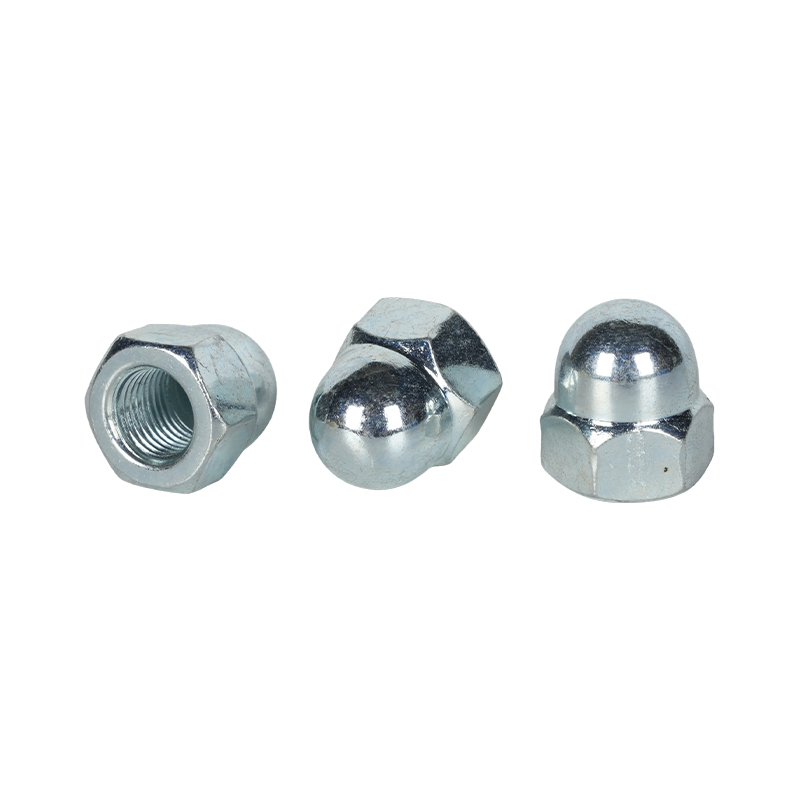
GB/T 802.3 Flange Domed Cap Nut
-
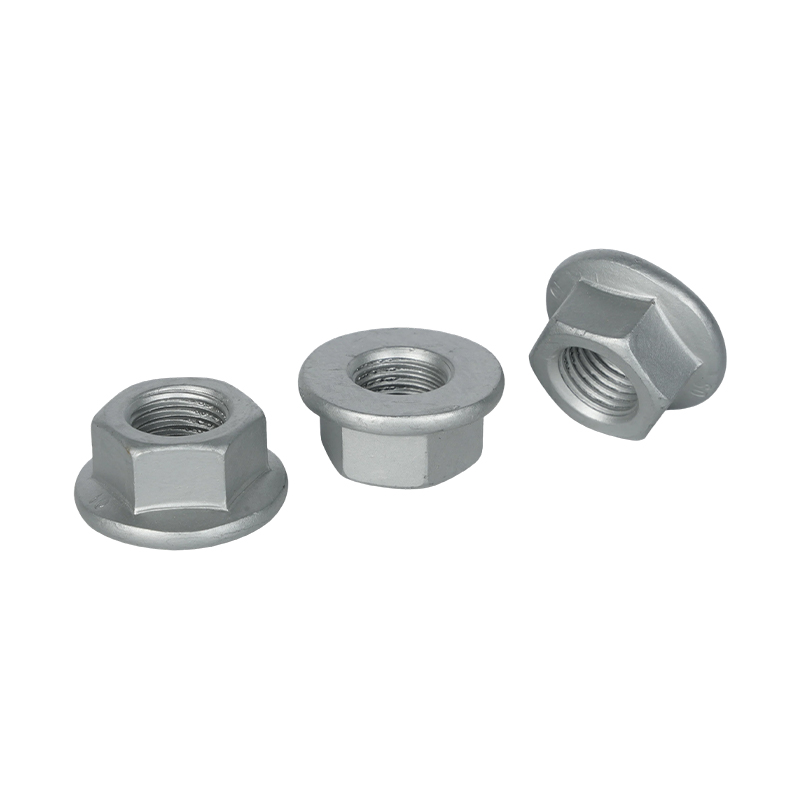
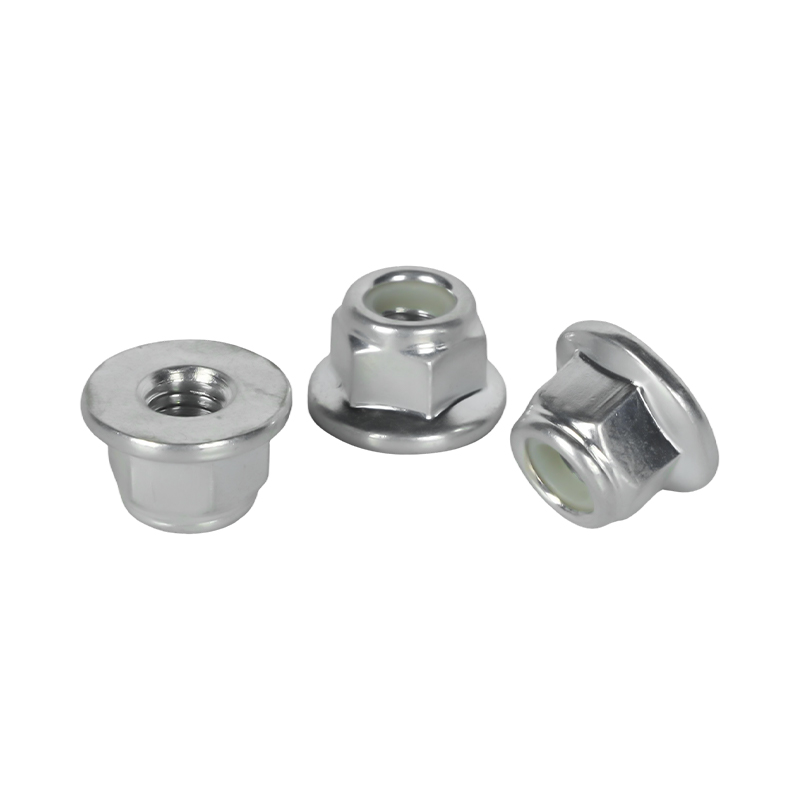
GB/T 6177 Hexagon Nuts with Flange,/DIN6923 Flange nuts with/without serration
-
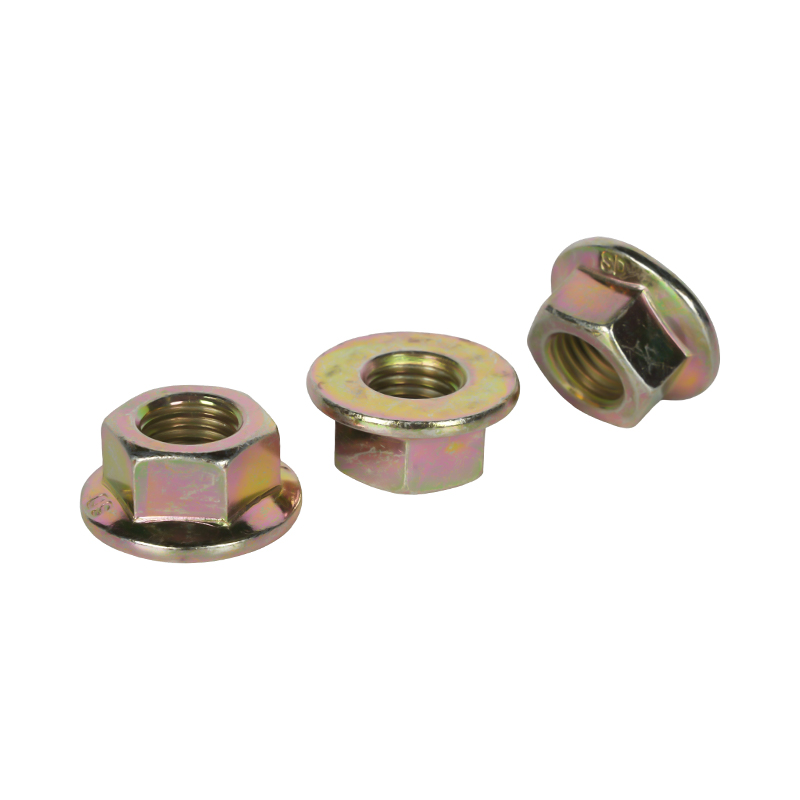
GB/T 6177 Serrated Hexagon Nuts with Flange, /DIN6923 Flange nuts with/without serration Yellow Zinc Plated
-
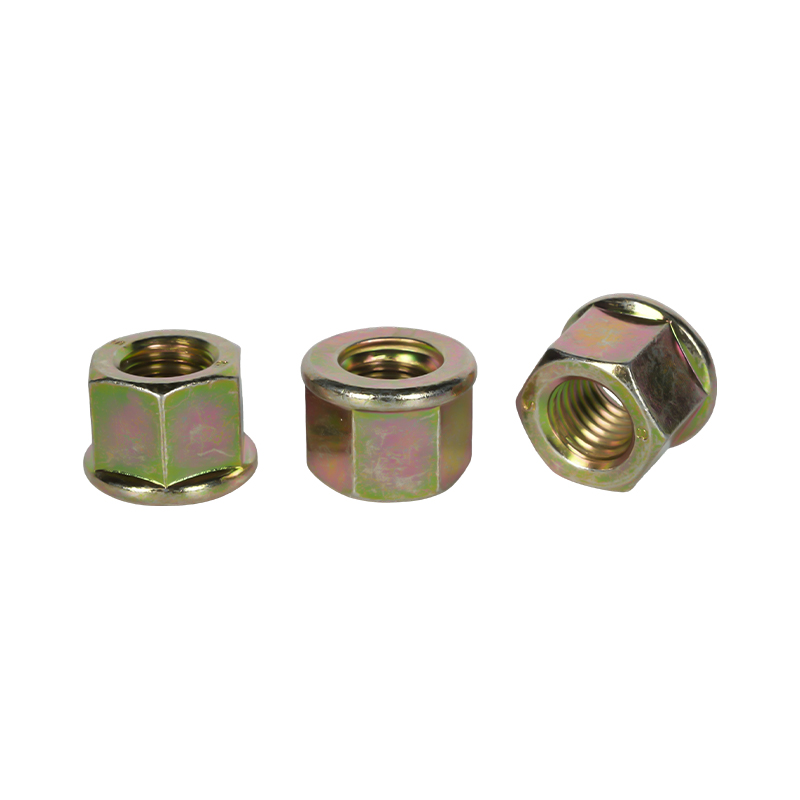
Thick Hex Flange Nuts, Yellow Zinc Plated
-
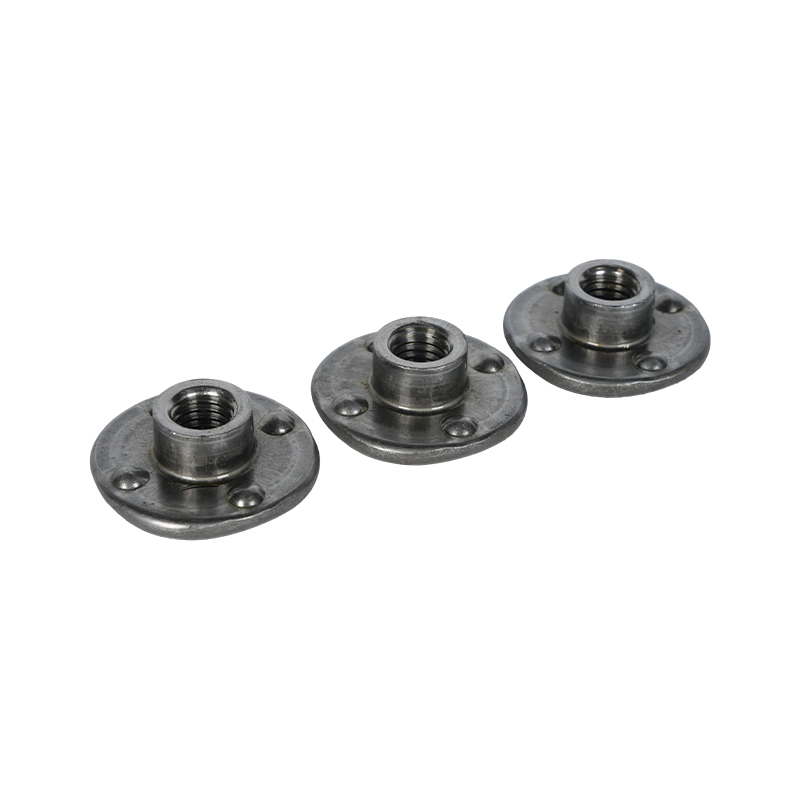
Spot Weld T- Nut
-
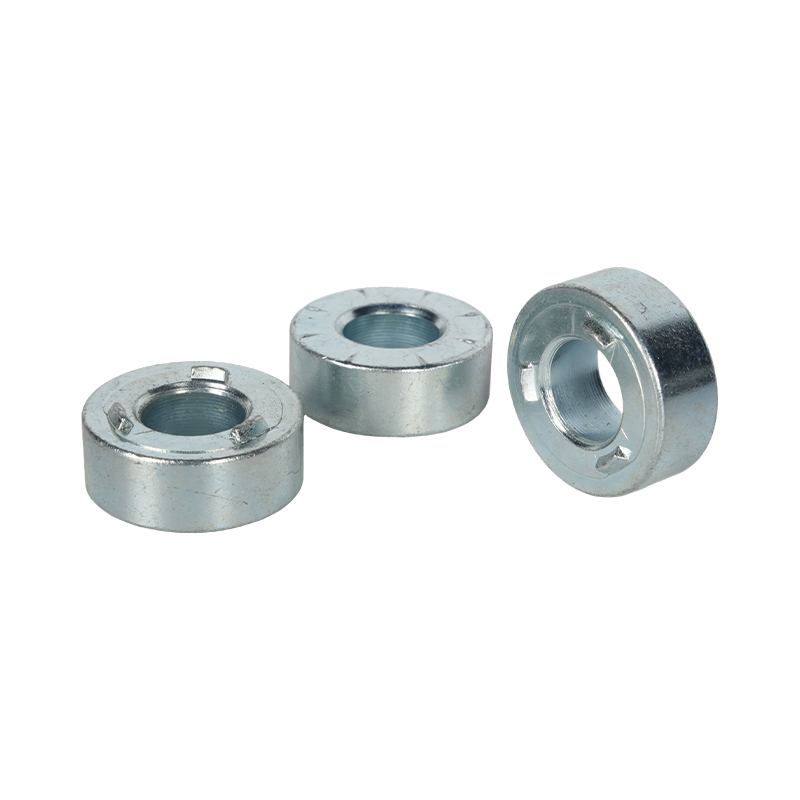
Round Weld Spacer, Zinc Plated
-
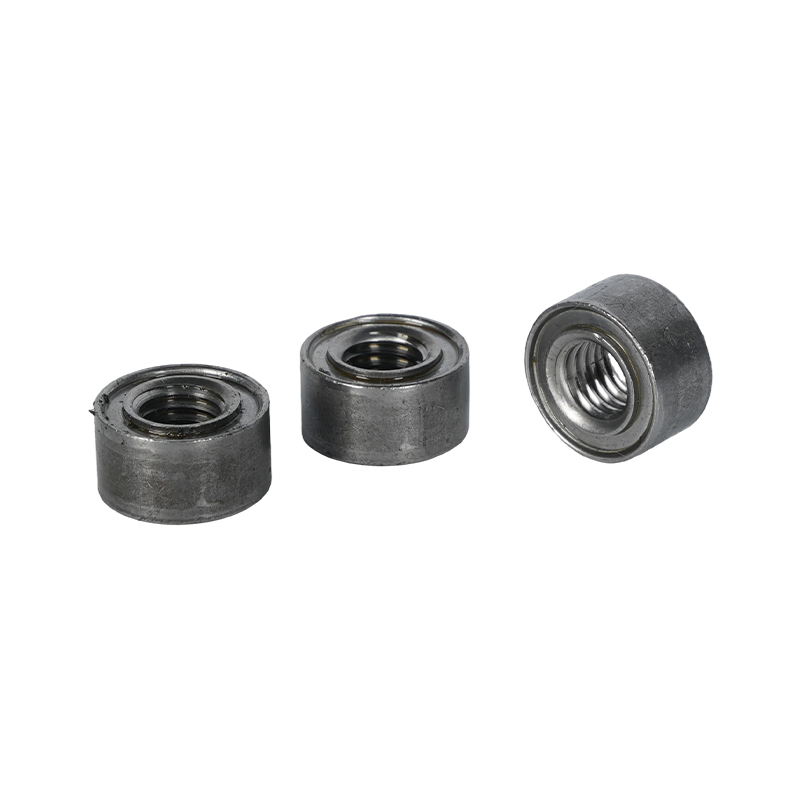
Round Weld Spacer with Internal Thread
-
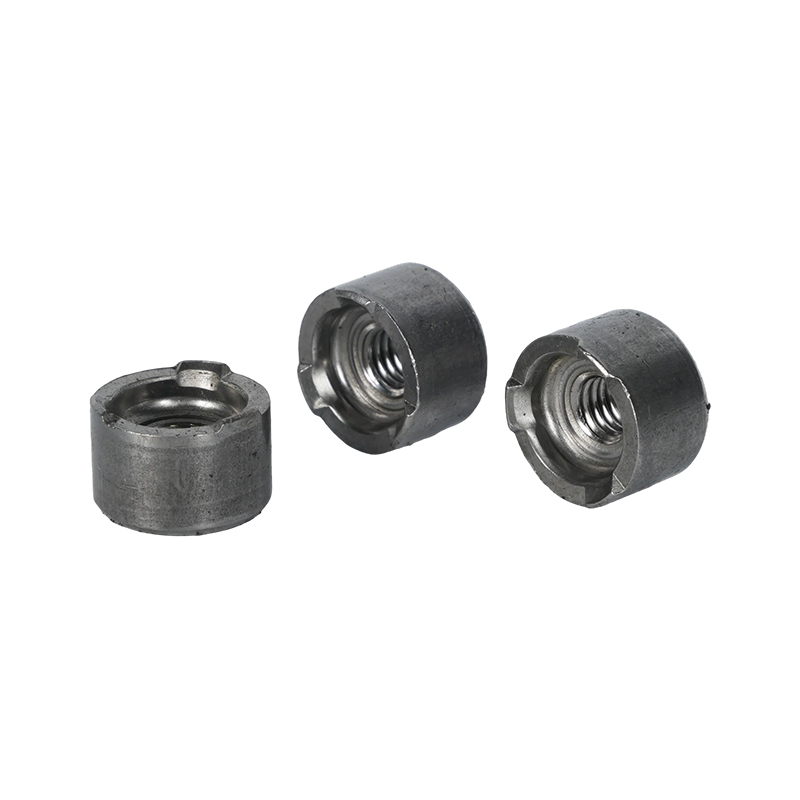
Carbon Steel Round Welded Nut, Cylindrical Welding Nut
-
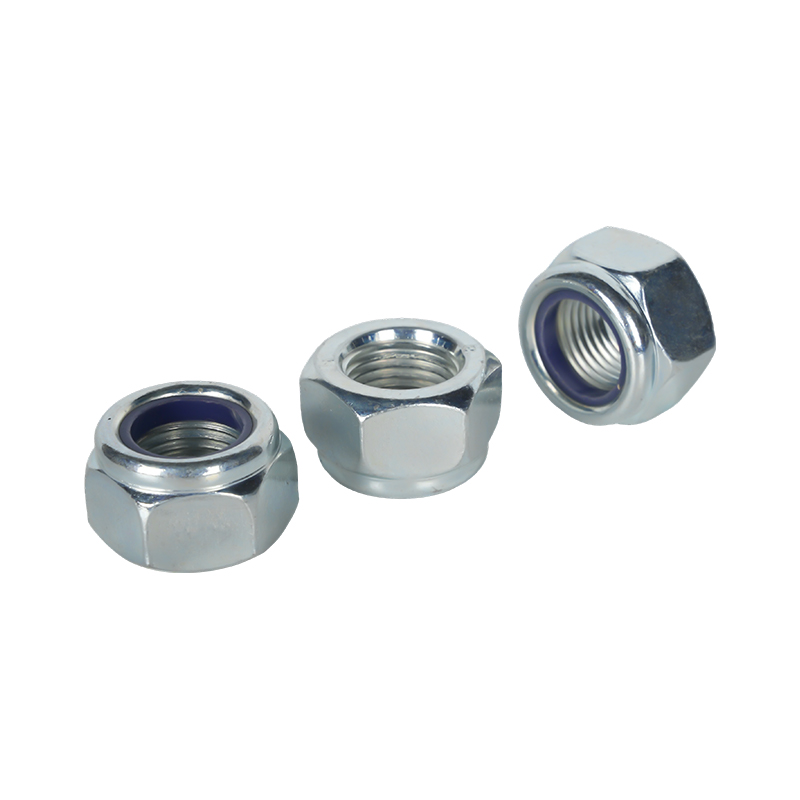
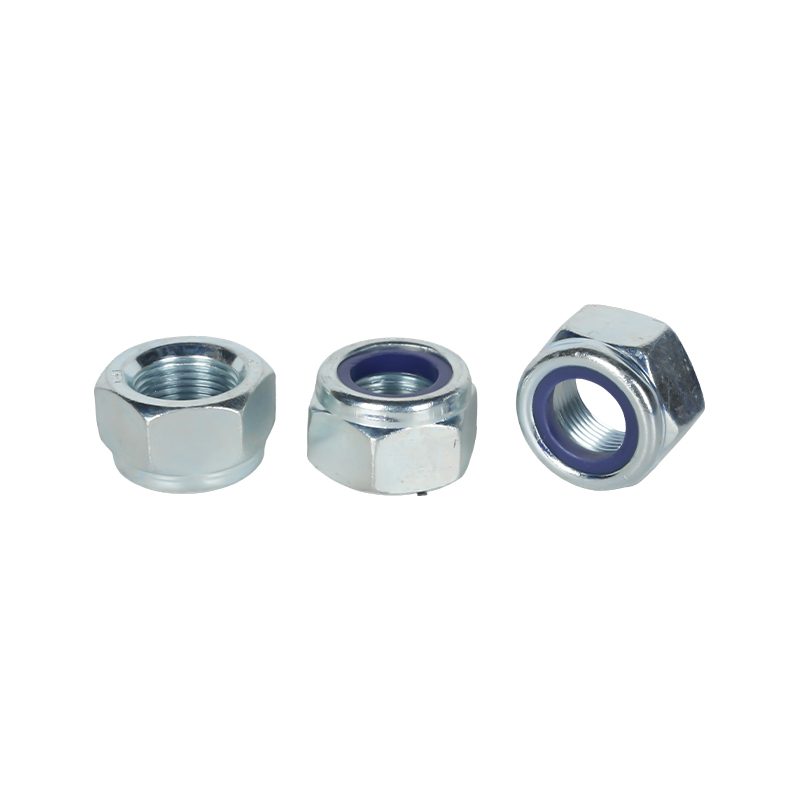
GB/T 6182 Hexagon Nuts with Non-Metallic Insert (Type 2)
-
GB/T 6183 Hexagon Nuts with Non-Metallic Insert (Type 1)/Nylon Insert Lock Nuts
-
GB/T 6182 Hexagon Nuts with Non-Metallic Insert (Type 2)/Nylon Insert Lock Nuts
-
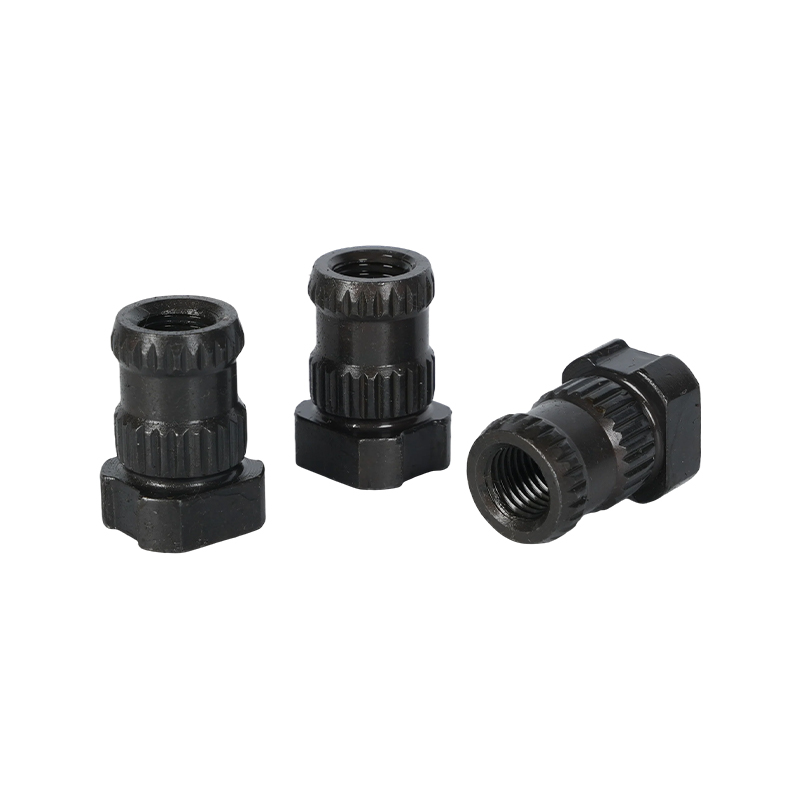
Black Carbon Steel Knurled Serrated Nut
Message Feedback
About Us
30 Years of Expertise in Automotive Fasteners
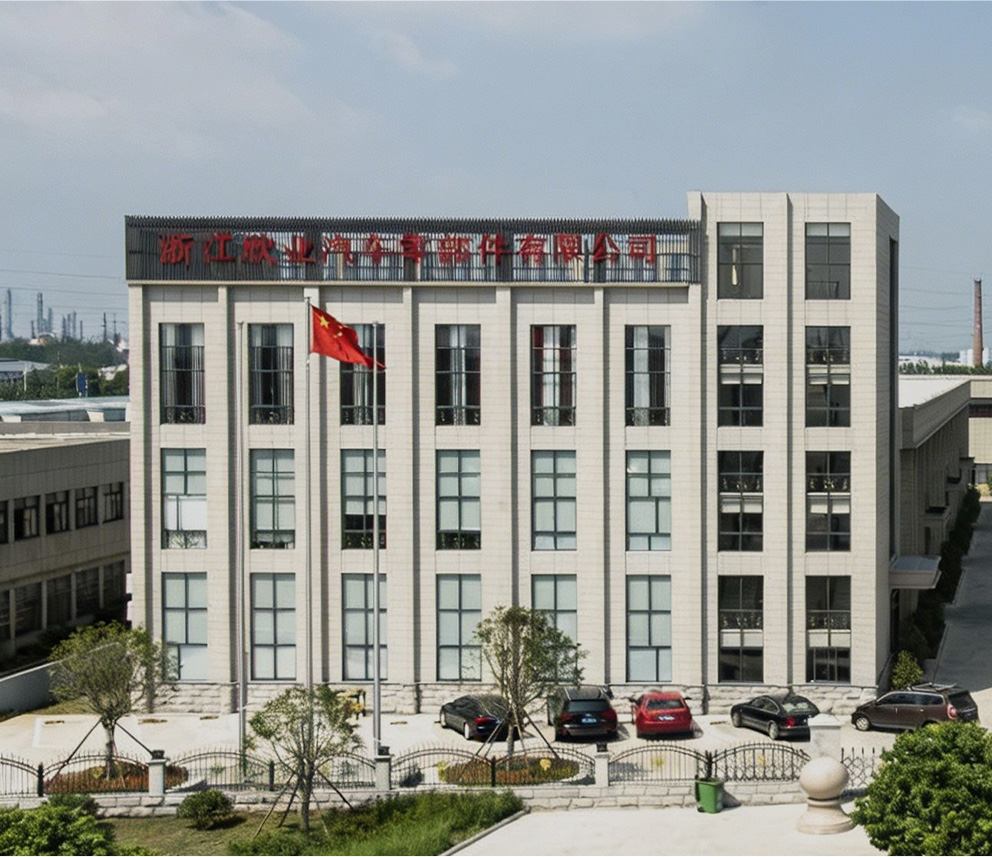
Zhejiangxinye Automobile Technology Co. , Ltd. traces its origins to 1995, evolving from Jiaxing Zhapu Xinye Standard Parts Co., Ltd. We are China Auto Body Nuts Suppliers and Custom
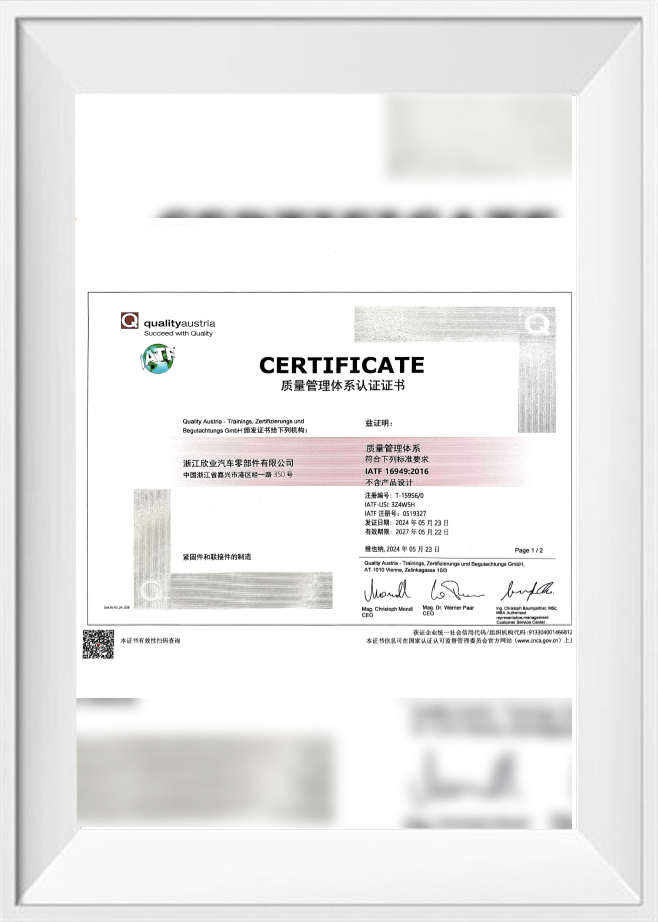
Auto Body Nuts factory. The company specializes in the production of various automotive fasteners and stamping parts, including flange nuts, welding nuts, and more. For over 30 years, Xinye has kept pace with industry trends, focusing on technological innovation and internal management, and has achieved steady growth. The company is now certified to IATF 16949-2016.
Adhering to the principle of "surviving by product quality, developing by technological innovation," Xinye takes quality as its foundation and customer satisfaction as a top priority, committed to providing suitable and reliable products. To enhance product competitiveness and strengthen employee quality awareness, the company has established a sound management system and standardized process flows. Work instructions have been developed for special and critical processes, and strict quality inspections are conducted at every step. From raw material analysis to finished product mechanical performance testing, process control is implemented to ensure product conformity. The continuously improving quality management system and stable product performance have earned the company market recognition, as well as customer trust and praise.
Adhering to the principle of "surviving by product quality, developing by technological innovation," Xinye takes quality as its foundation and customer satisfaction as a top priority, committed to providing suitable and reliable products. To enhance product competitiveness and strengthen employee quality awareness, the company has established a sound management system and standardized process flows. Work instructions have been developed for special and critical processes, and strict quality inspections are conducted at every step. From raw material analysis to finished product mechanical performance testing, process control is implemented to ensure product conformity. The continuously improving quality management system and stable product performance have earned the company market recognition, as well as customer trust and praise.
-
0m2
Factory Area
-
0
Brand Origin
-
0+
Product Range
Zhejiangxinye Automobile Technology Co. , Ltd.
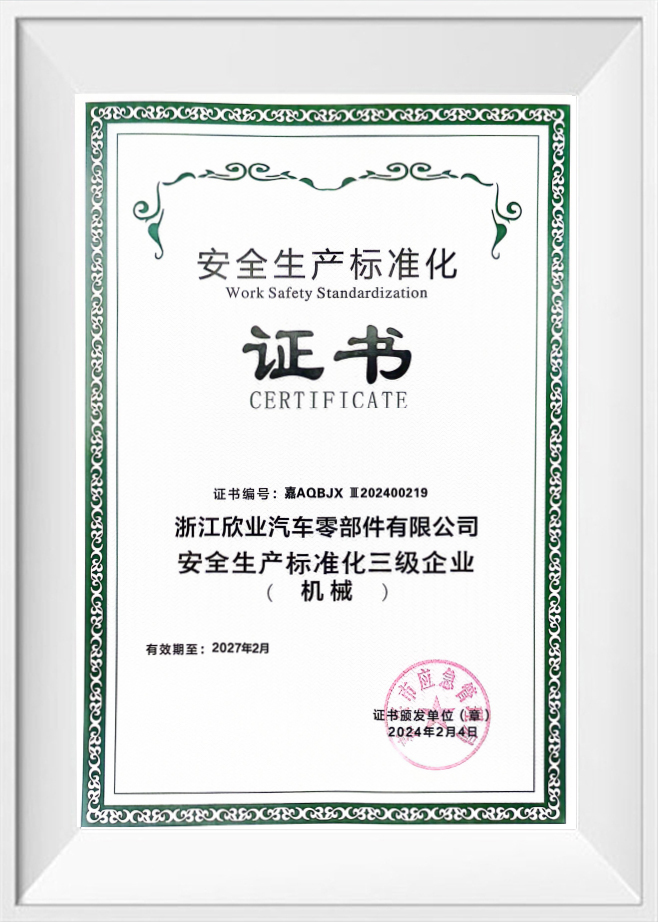
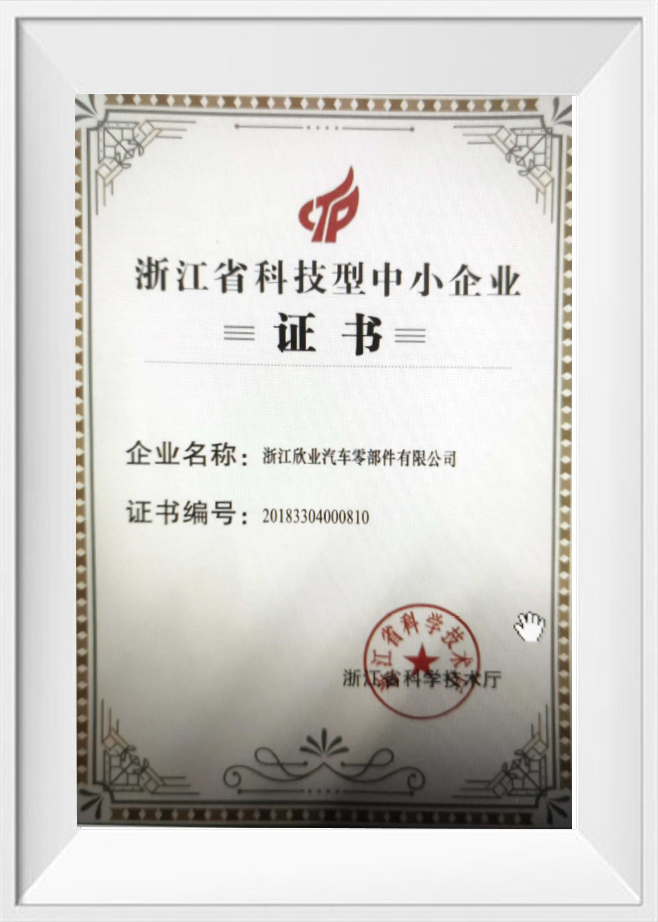
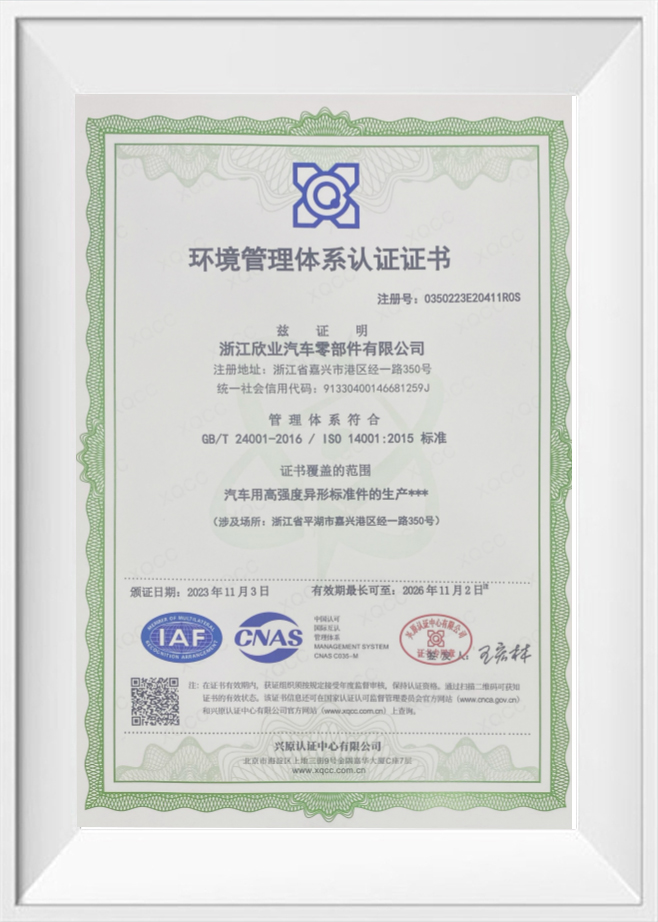
Certificate Of Honor
What’s News
Industry Insights & Updates
View All News
-
2026-11-03Industry News
-
2026-11-03Industry News
-
2026-11-03Industry News
-
2026-11-03Industry News
Nuts Industry Knowledge
Zhejiangxinye Automobile Technology Co., Ltd. manufactures custom auto body nuts for body-in-white, chassis, seat structure, interior trim and EV battery pack assemblies. Our nut programme carries 27 current configurations across eight families, from flange and hex nuts to weld, self-locking, knurled, slotted, clinch, sliding and fully drawing-specific parts, produced at our Jiaxing Port Area plant under IATF 16949-2016.
The business began in 1995 as Jiaxing Zhapu Xinye Standard Parts Co., Ltd. and has stayed in automotive fasteners since, adding stamping and machined component capacity alongside the nut lines. More than 500 fastener and stamping varieties now run through the same production and inspection system, with cold heading, tapping, heat treatment, thread rolling and surface finishing completed in-house.
Nut Families We Manufacture
As a Custom Auto Body Nuts Suppliers, Exporter - Zhejiang Xinye, we match product configuration to the application, operating limits, interfaces and acceptance criteria defined for each project.
Each family below is offered as a standard catalogue line and as a drawing-controlled variant, so a body programme can combine catalogue parts on general joints with purpose-built nuts on critical interfaces.
| Product range | Typical fit on the vehicle | Configuration focus |
|---|---|---|
| Standard Nuts | Flange and hex nuts on body brackets, cross members and general threaded joints | Flange diameter, serration, property class, coating |
| Weld Nuts | Body-in-white, closed sections, reinforcements and weld spacers where rear access is impossible | Weld projection geometry, pilot, thread depth, plating compatibility with welding |
| Self-Locking Nuts | Vibration-loaded joints on seat frames, suspension links, chassis and trim | Non-metallic insert type, prevailing torque, reuse behaviour, insert temperature limit |
| Knurled Nuts | Overmoulded plastic bosses, insert nuts and hand-adjustment points | Knurl or serration pattern, interference for the plastic, flange style |
| Slotted Nuts | Pin-retained and castellated adjustment joints | Slot width and depth, matching cotter pin, thread class |
| Clinch Nuts | Thin sheet metal brackets and panels installed after forming | Hole size, clinch geometry, sheet thickness range, push-out and torque resistance |
| Non-Standard Nuts | Drawing-specific joints with special steps, tabs, closed ends or mixed geometry | Full drawing control, material grade, tolerance band, secondary operations |
| Sliding Nuts | Adjustable joints and assemblies that must absorb build tolerance | Float range, cage or tab design, panel thickness, retention force |
As Custom Auto Body Nuts Suppliers, we quote from your drawing, standard reference or physical sample and confirm material, property class, thread and finish before tooling is released.
Where Our Nuts Fit on the Vehicle
Selection usually follows the joint, not the catalogue. The list below shows how we match each family to the assembly method and the access the line actually has.
- Body-in-white and closures: projection and spot-weld nuts, round weld spacers and cylindrical welded nuts handle closed sections and reinforcement points where a loose fastener cannot be reached.
- Thin sheet brackets: clinch nuts are pressed in after forming and hold on the panel without welding heat or rear access.
- Vibration-loaded joints: Self-Locking Nuts with a non-metallic insert keep preload on seat frames, suspension and trim fixings.
- Plastic and trim interfaces: knurled and serrated nuts grip the moulded boss and resist rotation during tightening.
- Adjustment points: slotted and sliding nuts leave room for pin locking or float, so assembly tolerance is absorbed at the joint rather than in the fixture.
For welded assemblies we review the welding process together with the nut, because projection height, pilot diameter and coating all influence weld quality and spatter behaviour.
Material, Strength Class and Thread Precision
Nuts are produced in carbon steel to the property class the joint requires, with classes matched to the mating bolt and the clamp load the assembly is designed to hold. Our strength development has moved from early Class 5 and 8 parts to Class 12 in series production, and higher grades are under active pre-research for heavy-duty and high-performance applications.
- Dimensional tolerance: controlled from 0.06 mm to 0.30 mm depending on the feature and the application, with the tighter band applied to pilot and thread-critical dimensions.
- Thread fit: tapping and thread rolling are set to the specified class, and go/no-go gauging is applied in process rather than at the end of the run.
- Heat treatment: in-house lines harden and temper to the requested class, verified with hardness testing before finishing.
- Closed ends and special geometry: available on non-standard parts where the joint calls for a sealed or guided thread entry.
Surface Finishing and Temperature Performance
Finishing runs on an in-house line, so coating thickness, coverage and hydrogen-related handling are controlled under the same system as the threads. Where a nut sits near the exhaust or engine, we supply high-temperature grades that hold their properties beyond the range of standard zinc finishes.
| Specification area | What we produce | Where it is used |
|---|---|---|
| Property class | Class 5 and 8 baseline, Class 12 in series production | Body, chassis and seat structure joints |
| Trivalent zinc plating | 480 h salt spray | General body and underbody fastening |
| Zinc-nickel alloy plating | 480 h to 720 h salt spray | Higher-corrosion chassis, wheel-end and exposed areas |
| High-temperature grades | 300 °C, 550 °C and 650–700 °C variants | Exhaust systems and engine periphery |
| Colour and appearance | Clear, yellow and black finishes across plating and coating routes | Visible trim fixings and underbody parts |
Assembly Line Integration and the MAT Thread
Automated tightening has little tolerance for cross-threading, especially on multi-spindle stations and robot cells where a single misaligned start stops the cycle. Our MAT thread technology adds a self-correcting lead on the first threads: if the bolt enters slightly off-axis, the nut guides it back into the correct thread path instead of cutting a new one.
This matters most on weld nuts inside closed sections and on clinch nuts in thin panels, where the operator cannot see or feel the start of the thread. We also set chamfer, pilot and thread run-out so the nut works with the socket, stud and feed system already on your line.
Quality Control and Acceptance Evidence
Production is covered by an IATF 16949-2016 quality management system, supported by work safety standardization and environmental management certification. Process control runs from incoming material to finished performance testing rather than relying on final inspection alone.
- Raw material: chemical analysis and incoming checks before the steel reaches heading.
- Special and critical processes: written work instructions with defined parameters, with inspection at each step.
- In-process verification: dimensional checks, thread gauging and hardness testing on equipment held in-house.
- Finished parts: mechanical performance testing and coating verification against the agreed specification.
Inspection results are recorded against the order so a repeat release references the same specification as the original build.
Information We Use to Configure Your Solution
We prepare a nut proposal from the joint data rather than from a part name alone. The following inputs let us fix material, geometry, coating and inspection scope in one pass.
- Drawing or standard reference, including thread size, pitch and class
- Mating bolt grade, target clamp load and tightening method
- Assembly method: projection weld, spot weld, press-in, overmould or manual fastening
- Panel or boss thickness and available rear access
- Coating, salt-spray target and any temperature requirement
- Annual volume, release pattern and packaging format
- Any marking, traceability or documentation required at part level
Current Production Highlights
Our catalogue includes flange nuts to GB/T 6177 and DIN 6923 with and without serration, GB/T 802.3 flange domed cap nuts, thick hex flange nuts in yellow zinc, and nylon-insert lock nuts to GB/T 6182 and GB/T 6183. Welded parts include the spot weld T-nut, zinc-plated round weld spacers and carbon steel cylindrical welded nuts, while knurled and serrated black carbon steel nuts cover plastic and trim interfaces.
Where a catalogue part does not fit the joint, our Non-Standard Nuts line covers stepped, flanged, tabbed and closed-end designs built to your drawing. Welded assemblies are supported by the full Weld Nuts range, from T-nuts to cylindrical spacers.
Frequently Asked Questions
Which nut families can Xinye supply for an auto body project?
Eight families: standard, weld, self-locking, knurled, slotted, clinch, non-standard and sliding nuts, with 27 configurations currently listed and further drawing-specific variants built on request.
Can you produce nuts to our drawing instead of a national standard?
Yes. Our non-standard line is built from customer drawings covering special steps, flanges, locating tabs, closed ends and mixed geometry, with material, property class and coating confirmed in the proposal.
What strength classes and tolerances do you hold?
Series production currently reaches Class 12, with Class 5 and 8 as the baseline for general body joints and higher grades in pre-research. Dimensional tolerance is controlled between 0.06 mm and 0.30 mm according to the feature and application.
How is corrosion protection specified?
We plate in-house with trivalent zinc at 480 h salt spray or zinc-nickel alloy at 480 h to 720 h, and supply high-temperature grades at 300 °C, 550 °C and 650–700 °C for exhaust and engine-adjacent positions.
How does the MAT thread help automated assembly?
The first threads are formed to correct a slight bolt misalignment and guide it into the correct thread path, which reduces cross-threading stoppages on robot cells and multi-spindle tightening stations.
What do you need to prepare a quotation?
A drawing or standard reference, mating bolt grade and tightening method, assembly process, panel thickness, coating and temperature requirements, annual volume and any marking or documentation needs. Send these to our Jiaxing Port Area team and we will return a configured proposal.
- Contact Us
-
-
861260628@qq.com

zj@xy-nuts.com -
+86 15888350558

-
No.350 Jingyi Road, Jiaxing Port Area, Zhejiang Province, China.

-
- Quick Links
- Products
- About Us
- Capabilities
- Service
- News
- Contact Us
- Product
- Nuts
- CNC Machined Components, Sleeves & Pins
- Specialty & Functional Automotive Components
- Metal Stampings
- Bolts & Screws
- Mobile
Copyright ©
Zhejiangxinye Automobile Technology Co. , Ltd.
All Rights Reserved
Custom
Auto Body Nuts Suppliers
